Steel beams are made in two stages. At the mill, steel is melted (usually from recycled scrap), cast into a thick semi-finished shape, reheated and hot rolled through a series of stands that squeeze it into the I profile, then cooled, straightened, cut, tested and stamped with a heat number. At the fabrication shop, that plain mill length is cut, drilled, fitted with plates and welded into the specific beam your drawings call for. This post follows a beam through both stages.
If you want to know which companies roll beams in North America, see who makes steel beams in Canada. This post is about the process.
What I-beams are made of
A structural beam is made of hot-rolled carbon steel: mostly iron, with a small amount of carbon, some manganese for strength and toughness, and limits on elements such as sulphur and phosphorus. The exact chemistry and the minimum strength depend on the grade.
In Canada, the wide-flange beams (W-shapes) used in buildings are commonly supplied to:
- CSA G40.21 350W, the Canadian structural grade, minimum yield strength 350 MPa
- ASTM A992, the US specification written for W-shapes, minimum yield 345 MPa (50 ksi)
Many mills certify beams to both at once. Our post on structural steel grades in Canada covers the grades in more detail.
People say "I-beam" for any steel beam, but most beams used today are W-shapes (wide flange) with parallel flanges, rather than the older S-shapes (American Standard beams) with tapered flanges. The difference is explained in I-beam vs W-beam vs H-beam. Both are made the same way.
Step 1: Making the steel
Structural mills in North America mostly use electric arc furnaces (EAF). The furnace is charged with scrap steel, sometimes with other iron sources, and huge graphite electrodes melt it with an electric arc. Steel is one of the most recycled materials there is, and much of a typical beam was once cars, appliances and old structures.
The other route is the integrated mill: iron ore is reduced to iron in a blast furnace, then converted to steel in a basic oxygen furnace. Both routes produce steel that can meet the same structural grades.
After melting, the steel goes to a ladle furnace, where the chemistry is adjusted. Alloying additions bring carbon, manganese and other elements into the range for the grade, and impurities are reduced. A sample is analysed so the heat (the batch of steel from one melt) can be certified.
Step 2: Casting the semi-finished shape
The refined steel is cast continuously: it pours into a water-cooled mould and is drawn out as a solid strand that is cut into lengths. For beams, mills cast either:
- Beam blanks, a near-net shape that already looks like a thick, rough "dog bone" version of an I-beam, which means less rolling to reach the final shape, or
- Blooms, thick rectangular sections that need more rolling passes.
Every piece is tracked by its heat number from this point on. That number follows the steel all the way to your job site.
Step 3: Hot rolling the beam profile
The blanks are reheated in a furnace until they are hot enough to be shaped, then rolled. Rolling a W-shape is done in stages:
- Breakdown or roughing. The blank passes back and forth through heavy rolls that start forming the web and flanges and reduce the section toward its final size.
- Universal rolling. A universal mill stand has horizontal rolls that work the web and the inside faces of the flanges, and vertical rolls that press on the outside faces of the flanges. Working both at once is what gives a wide-flange beam its parallel flanges and consistent thickness.
- Edging. An edger stand trims and controls the flange width and the shape of the flange tips.
- Finishing. Final passes bring the section to its exact size within rolling tolerances.
The same mill can roll many sizes within a nominal depth by changing the roll gap: a heavier beam in a family has thicker flanges and web and a slightly different overall depth. That is why a W250 family covers several masses per metre. See how to read steel beam sizes for what the designation means.
Step 4: Cooling, straightening, cutting and testing
After rolling, the long, hot section is sawn into manageable lengths and moved onto a cooling bed, where it cools in air.
Cooling unevenly leaves the beam slightly bowed, so it goes through a straightener, a set of rollers that bends it back within the straightness tolerance. Larger sections may also be straightened in a press. A small amount of natural curvature is allowed by the standard; our post on steel beam camber tolerances and natural mill camber explains how that is handled.
The beams are then cut to length by saw, usually to standard mill lengths or to lengths ordered by a service centre or fabricator. They are inspected for dimensions and surface defects, and test pieces are taken for mechanical testing (yield strength, tensile strength and elongation), with impact testing where the grade or order requires it.
Each beam is marked with the mill, size, grade and heat number, and the results are reported on a mill test certificate that ties the beam back to its chemistry and test results.
Built-up beams
Rolled sections stop at a maximum size. For deeper or heavier members, beams are made by welding plates together into an I shape: a web plate and two flange plates joined with continuous welds. In Canada these include the WWF (welded wide flange) shapes listed in the CISC Handbook, and fabricators also build custom plate girders. They are made in a fabrication shop or specialist plant rather than a rolling mill.
Step 5: From the mill to the fabrication shop
What leaves the mill is plain stock: no holes, no plates, no connections. It reaches a project through one of two routes:
- Steel service centres buy from mills, stock common sizes and sell them to fabricators in smaller quantities, sometimes cut to length.
- Fabricators buy large quantities directly from mills or through service centres for bigger projects.
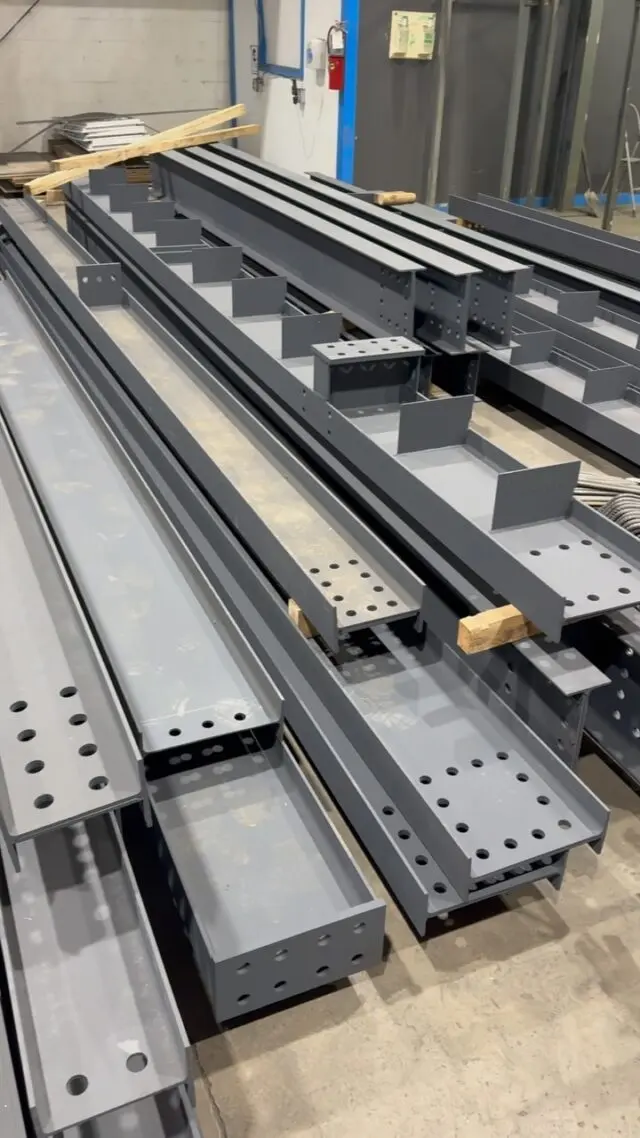
At the fabrication shop, the beam becomes a part of your building:
- Shop drawings detail every hole, plate, cope, weld and mark.
- Cutting to exact length, with copes or notches where the beam frames into another member.
- Drilling or punching holes for bolted connections.
- Fitting and welding plates, stiffeners, shear tabs and base or cap plates.
- Cambering if the drawings call for it.
- Cleaning and finishing: bare, primed or galvanized.
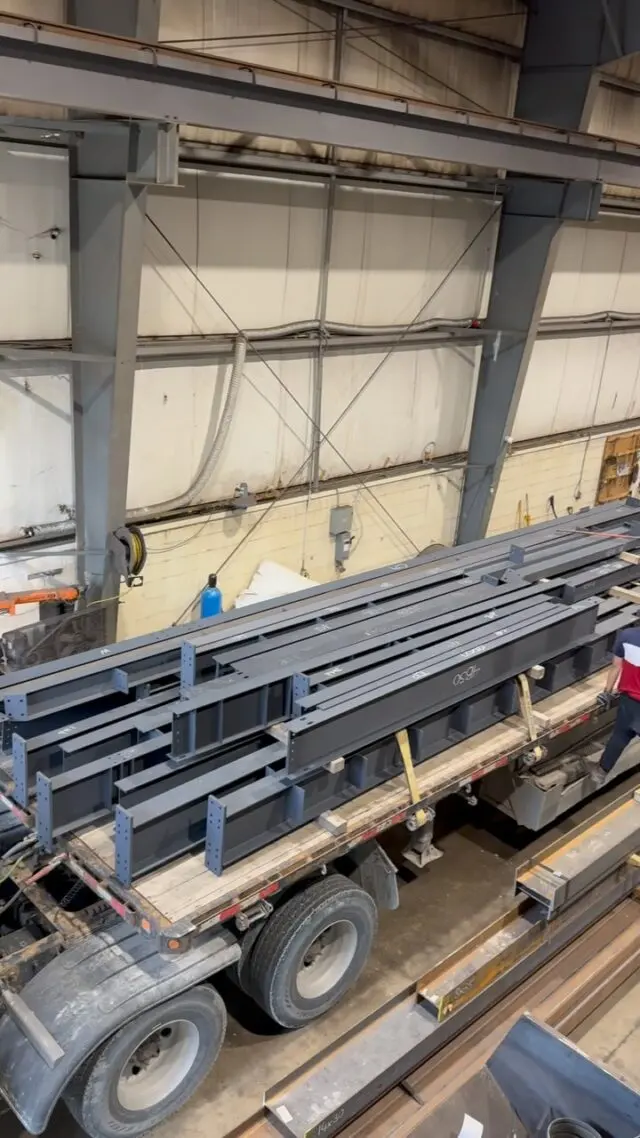
- Marking, loading and delivery to site.
Each of those steps is covered in detail in our post on how a steel beam is fabricated.
Tracing your beam back to the mill
For most structural projects, the engineer or inspector may ask for mill test certificates for the steel used. The heat number stamped or stencilled on the beam, recorded by the fabricator as the steel is cut, links the finished piece to its certificate. If a beam is cut into several pieces, good shops transfer the heat number or keep records so each piece stays traceable.
This matters when someone needs to confirm the grade: for instance, when an engineer specifies 350W and the beam was certified to A992, or when used steel of unknown origin turns up. Our post on reusing steel beams and offcuts discusses why unknown steel is a problem.
Get your beams fabricated
We take mill-certified beams and turn them into finished members: cut, drilled, welded with CWB certified shop welding, cambered where specified, primed or galvanized to suit, and marked to match the shop drawings we prepare in-house. Send your drawings through our quote request, or browse our steel products.
Frequently asked questions
How are steel I-beams made?
Steel is melted, usually from recycled scrap in an electric arc furnace, refined to the right chemistry and cast into a semi-finished shape called a beam blank or bloom. That is reheated and rolled through a series of mill stands that form the flanges and web, then cooled, straightened, cut to length, tested and marked.
What are I-beams made of?
Structural carbon steel: mostly iron, with a small amount of carbon and manganese and limited amounts of other elements. In Canada W-shapes are commonly supplied to CSA G40.21 350W and ASTM A992, often certified to both.
What type of steel is an I-beam?
A hot-rolled structural steel, not stainless or cast iron. The grade is shown on the mill test certificate. The most common grades for wide-flange beams in Canada have a minimum yield strength of about 350 MPa (50 ksi).
Are steel beams cast or rolled?
Standard beams are hot rolled. The steel is cast first into a semi-finished shape, but the final beam profile is formed by rolling. Very large or custom sections are built up by welding plates together instead.