Rebar fabrication is the shop process that turns straight bars from the mill into the exact reinforcing a concrete job needs: each bar is sheared to length, cold bent to its shape, tagged with its mark and bundled for delivery. It all runs from a bar list prepared from the structural drawings, so that what arrives on site is sorted, labelled and ready to place rather than raw stock your crew has to cut and bend.
Below is what happens between the mill and your formwork, step by step, and what "site-ready" should mean when you order fabricated rebar.
Where fabrication sits in the supply chain
Reinforcing steel passes through three hands before it is in the concrete:
- The mill rolls the steel into deformed bar to CSA G30.18, in standard sizes (10M to 55M) and grades, and in standard lengths. Under RSIC standard practice those are 12 m for 10M and 18 m for 15M and larger.
- The fabricator buys that bar, details the job if it is supplying the drawings, cuts and bends the bars to bar lists, tags and bundles them, and delivers.
- The placer (the reinforcing ironworker crew) installs the bars in the forms according to the placing drawings, and ties and supports them.
Rebar fabrication is the middle step. The Reinforcing Steel Institute of Canada's Manual of Standard Practice describes it as cutting, identifying, bundling, bending and loading reinforcing steel for transport, all to a specified bar list.
What goes in: bar, drawings and a bar list
Fabrication needs two inputs.
The material. Bar arrives from the mill in bundles. Each bar carries rolled-on marks identifying the mill, the bar size and the grade, with a W for weldable grades, repeated along its length. The mill also produces a mill test report for each heat of steel, giving its chemistry and mechanical properties. Under RSIC practice, a certified copy is provided at shipment when the buyer asks for it.
The bar list. Every fabricated bar comes from a line on a bar list: mark, quantity, size, grade, length and bend type with leg dimensions. The bar list is produced by detailing the structural drawings, either by the fabricator or by the contractor's own detailer. Before production starts, the shop needs the job information that ties each bar back to the project: the contract and order, the bar list, grade, mark, number of bars, size, length, the part of the structure and the bending required.
If the bar list is wrong, fabrication will reproduce the mistake perfectly. That is why the review of placing drawings and bar lists happens before release, not after delivery. Our post on what rebar detailing is explains how bar lists are built.
The fabrication steps
1. Shearing to length
The first shop operation is cutting each bar to its listed length, usually on a shear. The shop plans its cuts across the standard mill lengths to keep offcuts down. Straight bars are finished at this point: they are bundled, tagged and moved to shipping. Bars that need shape move on to bending.
2. Bending
Bent bars go to bending equipment and are cold bent to the bend type and leg dimensions on the bar list. Each bend is made around a pin sized to at least the minimum bend diameter for that bar size, which keeps the steel from cracking or being damaged. RSIC practice is that bars are not bent or straightened in a way that damages them.
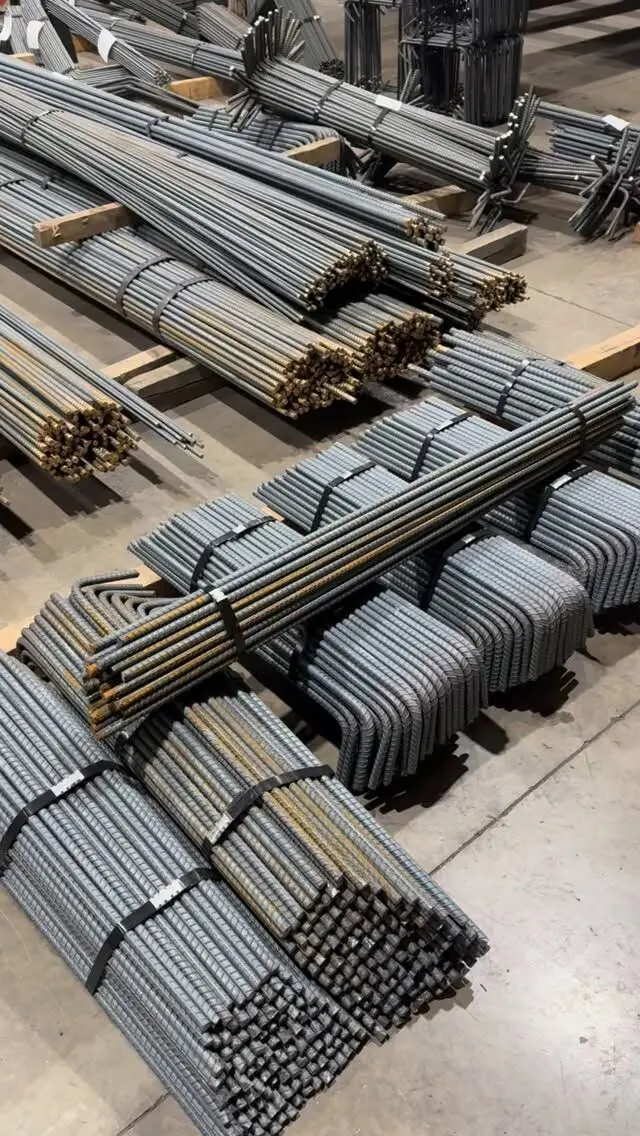
Common fabricated shapes include:
- Hooked bars with standard 90°, 135° or 180° hooks. See rebar hooks and bend radius.
- L-bars and corner bars for footings and wall intersections.
- Dowels that tie footings to walls or new concrete to old.
- Stirrups and ties that wrap the main bars in beams and columns.
- Custom shapes detailed on the bar list with a sketch.
Standard fabricating equipment bends in one plane, so a bar that would need bends in two planes is usually detailed as two bars spliced together. That is cheaper to make and easier to place. RSIC numbers the standard shapes as typical bar bends, and anything outside them is drawn as a sketch on the bar list.
3. Tagging and bundling
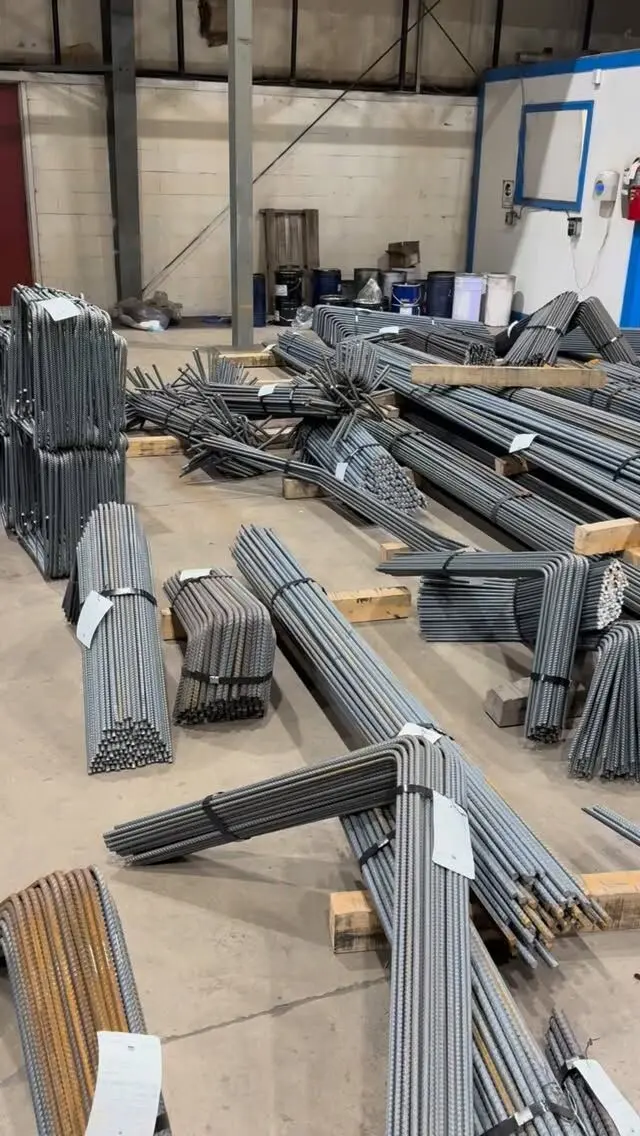
Every bundle gets a weather-resistant tag showing the job, the bar mark, size, quantity and length, and often the part of the structure. Under RSIC practice a bundle holds bars of one size and similar length, with small quantities grouped where it makes sense, and bundle weights are kept within what the shop and the site can lift. Some shops colour-code tags by element (footings, walls, slabs) so the crew can see at a glance where a bundle belongs.
4. Loading for delivery
Bundles are loaded in the order the job needs them, with the weight spread across the trailer and enough dunnage between layers to get slings or forks underneath. Delivery is usually planned by release or pour, so the steel for one pour arrives together.
Quality control in a rebar shop
RSIC's manual is frank that there is no industry-wide quality assurance standard for rebar fabrication. The responsibility for delivering the correct quantity, size, grade, length and shape rests on the fabricator. In practice, good shops build their checks into each step:
- Material traceability. Heat numbers are linked to the parts of the structure they went into, either through production software and scanners or by the shear operator recording them by hand. That lets a mill test report be matched to a specific pour.
- Dimension checks on first pieces and during runs, against the tolerances in RSIC's fabricating standard practice. Our post on rebar fabrication tolerances lists them.
- Count and tag checks before bundles are loaded, so the tag matches the bars in the bundle.
- Revision control, so a superseded bar list never reaches the shop floor.
Coated, specialty and GFRP bar
Not every bar is plain black steel, and each type changes the fabrication:
- Epoxy-coated and galvanized bar need careful handling so bending and lifting don't damage the coating, and any damage is repaired as the specification requires.
- Welded reinforcing is a separate operation done to CSA W186 under CWB requirements, and it is simplest with a weldable (W) grade bar.
- GFRP bar can be cut to length, but it cannot be bent like steel once its resin has cured. Bent GFRP shapes are made by the manufacturer and ordered on the bar list. See GFRP corners, L-bars and hooks.
Shop fabrication vs cutting and bending on site
Small jobs sometimes buy straight bars and cut and bend them on site with a portable cutter and bender. That can work for a handful of simple bends. On anything larger, shop fabrication usually wins: bends are made to the right diameter on proper equipment, every piece is tagged, nothing is cut short by mistake, and the crew spends its time placing steel instead of making it. Our comparison of bending stirrups on site vs shop fabrication goes through the trade-offs.
Fabricated rebar from our Erin shop
We prepare reinforcing steel estimates, bar lists and placing drawings from your structural drawings, then shear bars to length, bend them to all standard shapes, and tag and bundle them so your crew can place them without sorting on site. We fabricate 10M to 55M bar, including dowels, stirrups, ties and custom bent shapes, supply GFRP rebar, and deliver across the GTA and Ontario with phased deliveries to match your pours.
Send us your drawings or bar list for a free take-off and quote, or see our rebar products.
Frequently asked questions
What is rebar fabrication?
Rebar fabrication is the shop work that turns straight mill bars into the exact pieces a concrete job needs: bars are sheared to length, cold bent to shape, tagged with their mark and bundled for delivery, all to a bar list prepared from the structural drawings.
What is the difference between a rebar mill and a rebar fabricator?
A mill rolls the steel into straight bars in standard sizes, grades and lengths. A fabricator buys that bar, details the job, cuts and bends it to bar lists, tags and bundles it, and delivers it to site.
Is rebar bent hot or cold?
Cold. Canadian standard practice is that reinforcing bars are cold bent to the bar list dimensions, around pins sized to the minimum bend diameters, and are not bent or straightened in a way that damages the steel.
Can fiberglass (GFRP) rebar be fabricated in a rebar shop?
GFRP bars can be cut to length, but they cannot be bent like steel once cured. Bent GFRP shapes are made at the manufacturer and ordered as part of the bar list.