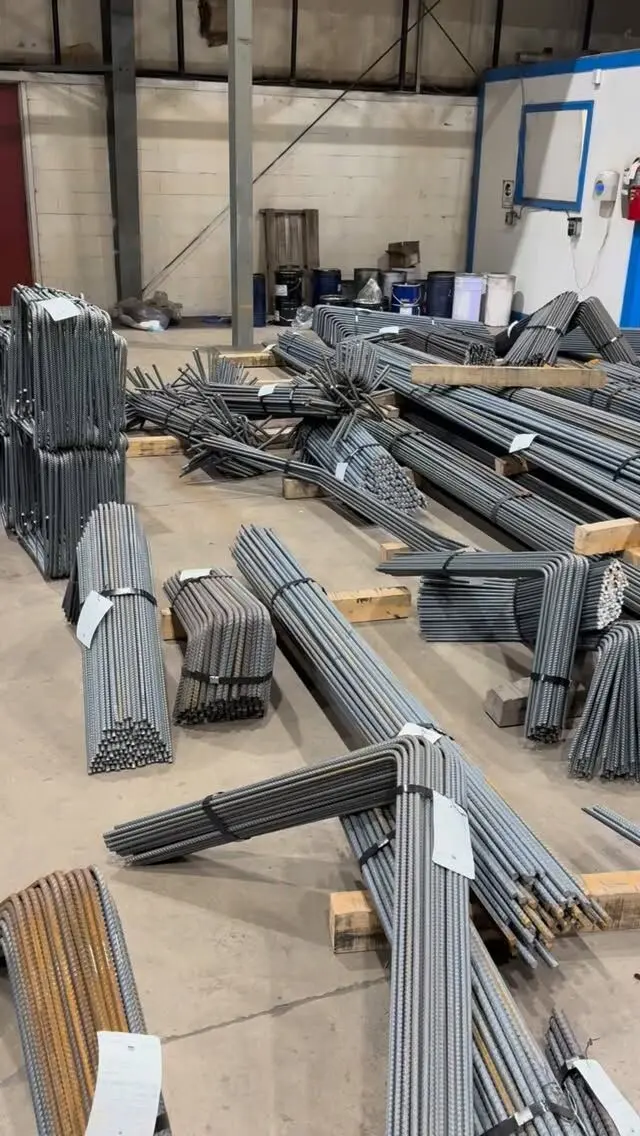
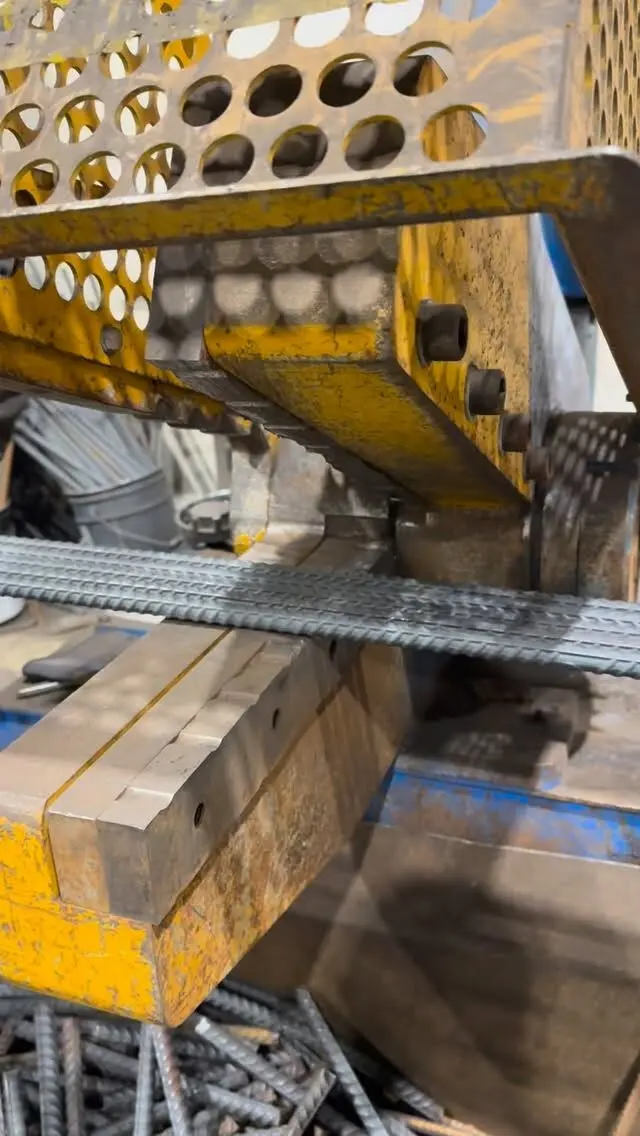
A rebar stirrup is made by cutting a bar to the stirrup's cut length, then cold bending each corner and hook around a pin of the right diameter until the out-to-out size matches the drawing. You can do that on site with a manual or portable powered bender, or have a fabricator bend them in the shop. For anything more than a handful of pieces, shop-fabricated stirrups are faster, more consistent and easier to inspect, and they arrive tagged by mark. Site bending makes sense for a few replacements or a piece that has to be fitted to conditions on site.
This post covers how stirrups are made and the trade-offs between bending them yourself and ordering them. For sizing, shapes and how to write the order, see our guide to ordering custom rebar stirrups.
How a stirrup is made
Whether it happens in the shop or beside the forms, the sequence is the same:
- Get the size from the drawings. Stirrups are dimensioned out-to-out: outside of one leg to outside of the other. If the drawings do not give a size, RSIC practice details stirrups 80 mm smaller than the beam in width and depth, but only use that when the cover on your job matches.
- Work out the cut length. Add the out-to-out sides and the hook allowance at each end. Our post on stirrup sizes and hook lengths gives the allowances (100 mm for 10M and 140 mm for 15M standard hooks) and a worked example.
- Cut the bar to that length.
- Bend each corner and hook around a pin of the correct diameter, in an order that keeps the shape square and the hooks where the drawing puts them.
- Check the first piece against the drawing: width, height, hook type and hook direction. Adjust before bending the rest.
The pin diameter is not a matter of preference. CSA A23.1 sets the minimum inside diameter for stirrup and tie bends at four bar diameters, and the RSIC tables translate that into a 45 mm pin for 10M and a 65 mm pin for 15M. Bending tighter than that, for example by levering the bar over a sharp edge, overstresses the outside of the bend.
Tools for bending stirrups on site
Manual benders. A lever bender mounted on a base or a bench, with a pin and a stop, is the basic site tool. It works for 10M and, with effort, 15M. Consistency depends on the operator setting marks and stops carefully for every bend.
Hickey bars. A notched bar used to bend rebar by hand. Handy for small adjustments, but it is hard to hold a controlled bend diameter with one, so it is a poor choice for making stirrups to a drawing.
Portable electric benders. Powered units, often combined with a cutter, take interchangeable pins and angle stops. They are faster and more repeatable than manual tools and reduce strain on the crew, but they are still bending one piece at a time.
Bending jigs. A plywood or steel table with pins set at the stirrup dimensions helps a crew turn out a batch of identical pieces. It is only as accurate as its layout.
Whatever the tool, the operator needs gloves, eye protection and a clear swing area. Bars can slip or spring back under load, and exposed bar ends need protective caps once the steel is in place.
How shops bend stirrups
A rebar fabrication shop bends stirrups on bending tables with fixed pin sets or on automatic stirrup benders that bend bar to programmed dimensions, piece after piece. The detailer's bar list sets the shape, size and hook for each mark, the bent pieces are bundled and tagged, and the bundle goes to site ready to place.
The standard of accuracy is set out in advance. Under RSIC standard practice, the fabricating tolerance for stirrups and ties is plus or minus 13 mm. Hooks are bent with the pin diameters and dimensions in the RSIC tables unless the engineer specifies otherwise, and bars must not be bent or straightened in a way that damages them.
Rules that apply wherever the bar is bent
The concrete standards do not care where a stirrup was bent, only that it was bent properly:
- Bend cold. CSA A23.1 requires bars to be bent within a set temperature range (10°C to 100°C in the 2004 edition) unless the owner permits otherwise. Heating a bar with a torch to make bending easier is not standard practice and needs the engineer's approval. In very cold weather, follow the bar supplier's and engineer's guidance.
- Use the right pin. At least four bar diameters inside for stirrup bends, and larger for the hooks on 20M and bigger bars.
- Do not rebend. Straightening a bent bar and bending it again, or reshaping a stirrup that does not fit, can crack or weaken the steel. Our post on whether bending rebar weakens it explains why.
- Leave embedded bars alone. A23.1 does not allow bars partly embedded in concrete to be field bent unless the drawings show it or the owner permits it (2004 wording; in practice, ask the engineer).
- Coated bar needs care. Epoxy-coated bars use larger bend diameters than black bar, and any coating damage at the bend has to be repaired.
- GFRP cannot be bent on site. Glass fibre reinforced polymer stirrups have to be made bent by the manufacturer. See GFRP stirrups and dowels vs steel rebar.
Site bending vs shop fabrication compared
| Factor | Bending on site | Shop fabricated |
|---|---|---|
| Accuracy | Depends on the tool and operator; drifts over a long run | Set by machine and pin set; RSIC tolerance of ±13 mm |
| Consistency between pieces | Varies, especially with manual tools | Repeatable across hundreds of pieces |
| Labour | Crew time spent cutting and bending instead of placing | Crew places stirrups straight from the bundle |
| Waste | Offcuts and miscut pieces on site | Cutting planned from the bar list in the shop |
| Identification | Pieces must be sorted and marked on site | Bundled and tagged by mark |
| Seismic or 135° hooks | Hard to get right with hand tools | Bent to the specified hook allowance |
| Inspection | More pieces to check by eye | Easier to verify against the bar list |
| Lead time | Immediate, if tools and bar are on hand | Needs a bar list and delivery |
The stirrup is the part of a rebar order with the least room for error. A stirrup 20 mm too large pushes the main bars into the cover; one 20 mm too small will not fit around them. That is why the Ontario Cast-in-Place Concrete Development Council (OCCDC) reference guide recommends that all reinforcing bars be shop fabricated, because the work can be done more accurately in the shop.
When bending on site makes sense
There are still good reasons to bend a few stirrups on site:
- Replacements. A bundle is short a few pieces, or some were damaged.
- Field fit. An existing structure or a late change means a dimension is only known once the forms are up.
- Very small jobs. A single pier, a short grade beam or a repair where a few pieces of 10M is all that is needed.
Even then, bend to the drawings, use a proper bender with the correct pin, and check every piece. If the reason for bending on site is that the shop stirrups do not fit, stop and find out why before you change anything. A wrong formwork dimension or a detailing error needs to be fixed at the source, and a different stirrup size is the engineer's call.
What drives the cost
Bending your own stirrups looks cheaper because the bar costs less than a fabricated piece. The real comparison includes crew hours at the bender instead of at the forms, tools, offcut waste, miscut pieces and the risk of rework at inspection. Fabricated stirrup cost depends on the total weight, the number of different marks, quantities per mark, hook types, any coating and delivery. Under RSIC estimating practice, stirrups and ties count as light bending and are priced separately from the bar itself. How rebar is priced explains how quotes are built.
Order stirrups bent to your drawings
We cut and bend stirrups, ties, crossties and dowels in our shop to your bar lists, or detail them from your structural drawings, and tag and bundle every mark. Send us your drawings or stirrup schedule and we will prepare a free take-off and quote; ask us about lead times for your job.
Request a stirrup quote or see our rebar products for fabricated rebar, straight bar and GFRP.
Frequently asked questions
How are rebar stirrups made?
The stirrup size comes from the drawings, the bar is cut to the stirrup's cut length, and each corner and hook is cold bent around a pin of the correct diameter, then checked against the drawing. Shops do this on bending machines; on site it is done with a manual or portable powered bender.
Can you bend stirrups on site?
Yes, for small quantities, provided the bars are bent cold around the correct pin diameter and the result matches the drawings. Bars already partly cast into concrete should not be field bent unless the drawings show it or the engineer permits it.
What tool is used to bend rebar stirrups?
On site, a manual rebar bender or a portable electric bender with interchangeable pins. In a fabrication shop, bending tables and automatic stirrup benders that bend bar to programmed dimensions.
Can you heat rebar to bend it?
Not as a routine practice. CSA A23.1 requires bars to be bent within a set temperature range unless the owner permits otherwise, and heating changes the steel. Bend cold with the right tool, or have the bars shop fabricated.
Is it cheaper to bend stirrups yourself?
Rarely, once labour, waste, tools and rework are counted. Shop bending is faster and more consistent, and the stirrups arrive tagged by mark. Site bending only pays on a handful of pieces or a field-fit situation.