Structural steel inspection is a series of checks from the mill to the finished frame: material and certificates, fit-up and dimensions, welds, bolts, coatings, marking, and erection. The fabricator's quality control does these checks on every job. Third-party inspection is added when the project specification calls for it, and on buildings that require it, the engineer carries out general review of construction under the Ontario Building Code. The checklist below follows the work stage by stage.
For the standards behind the checks, see steel fabrication standards in Canada.
Who inspects structural steel
Four kinds of review often get lumped together as "inspection." They have different jobs.
| Who | What they do | When it applies |
|---|---|---|
| Fabricator and erector quality control (QC) | Check their own work against the drawings and standards, and keep records | Every job |
| Third-party inspection (quality assurance) | Independent inspection and testing for the owner, often including non-destructive testing of welds | When the specification requires it |
| Engineer of record (general review) | Reviews construction for general conformity with the permit drawings and reports to the building official | Buildings where the 2024 OBC requires general review (Division C, Article 1.2.2.1) |
| Municipal building inspector | Inspects at the stages required under the building permit | Permit work |
CSA S16 makes the fabricator responsible for quality. It does not require a third-party inspector on every project. S16-19 includes an informative annex that lets the engineer choose an inspection class and set inspection frequencies, which applies when the specification adopts it. Our standards overview explains that annex in more detail.
Inspector certifications
- Welding inspectors are certified to CSA W178.2 by the CWB Group. The CWB describes Level 1 as entry level, working under Level 2 or 3 supervision; Level 2 inspectors are considered competent to inspect without supervision; Level 3 inspectors have additional technical knowledge for tasks such as inspection and test plan reviews.
- Inspection companies can be certified to CSA W178.1, which covers organizations providing visual and non-destructive inspection services.
- NDT technicians performing ultrasonic, magnetic particle, penetrant or radiographic testing hold method-specific certification.
When a specification names an inspection company or a certification level, ask for the certificates with the inspection reports.
Checklist: before fabrication starts
Most problems are cheaper to catch on paper.
- Shop drawings reviewed and returned, and the shop is working from the latest approved revision
- Erection drawings and anchor rod plan issued and consistent with the shop details
- Specification requirements captured: inspection, NDT, finish, camber, bolt type, slip-critical joints
- Fabricator's CWB certification to CSA W47.1 current (see why hire a CWB-certified fabricator)
- Welding procedure data sheets available for the joints on the job
- Welders qualified for the processes and positions they will use
- Hold points agreed with the third-party inspector, if there is one
Checklist: material
- Section sizes and plate thicknesses match the drawings
- Grade matches the specification (for example 350W, A992 or A500, as specified)
- Mill test certificates on file where traceability is required, matched to heat numbers on the steel
- Material free of damage, laminations, heavy pitting or excessive mill scale defects
- Any substitution (size or grade) approved by the engineer in writing
Grade substitutions are not a shop decision. CISC cautions, for example, that HSS to ASTM A500 is not an automatic substitute for CSA G40.21 350W of the same nominal size.
Checklist: fabrication and welding
Cutting, holing and fit-up
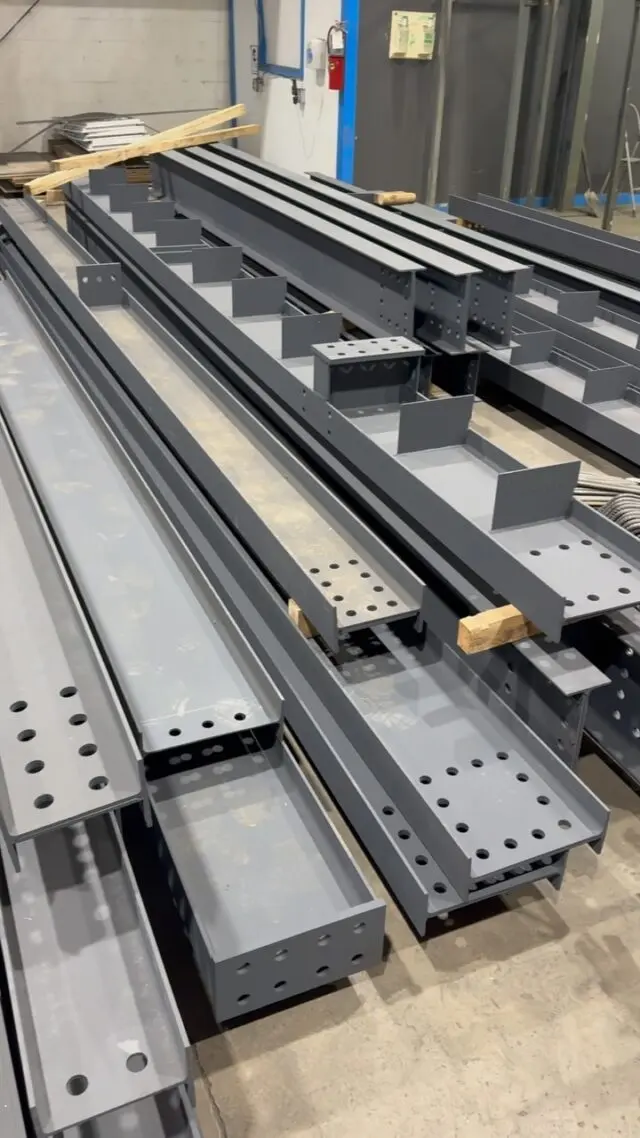
- Lengths, copes, bevels and end cuts match the details
- Hole sizes, gauges, pitches and edge distances correct
- Plates, stiffeners and clips located and oriented as detailed
- Joint preparation and root openings suit the welding procedure
- Camber, where specified, measured and recorded
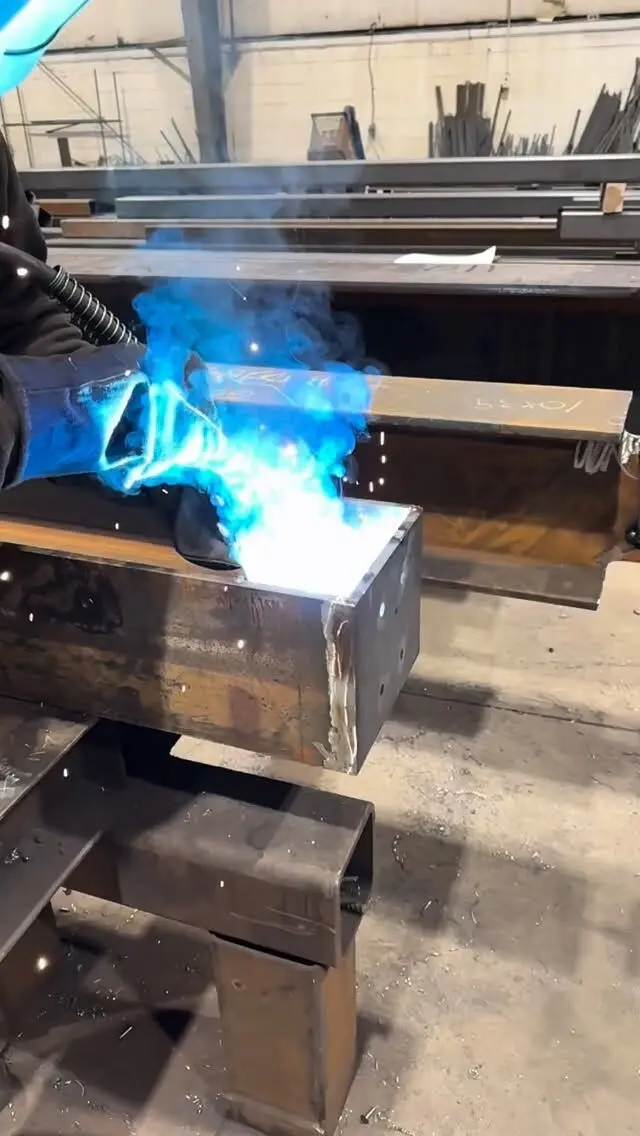
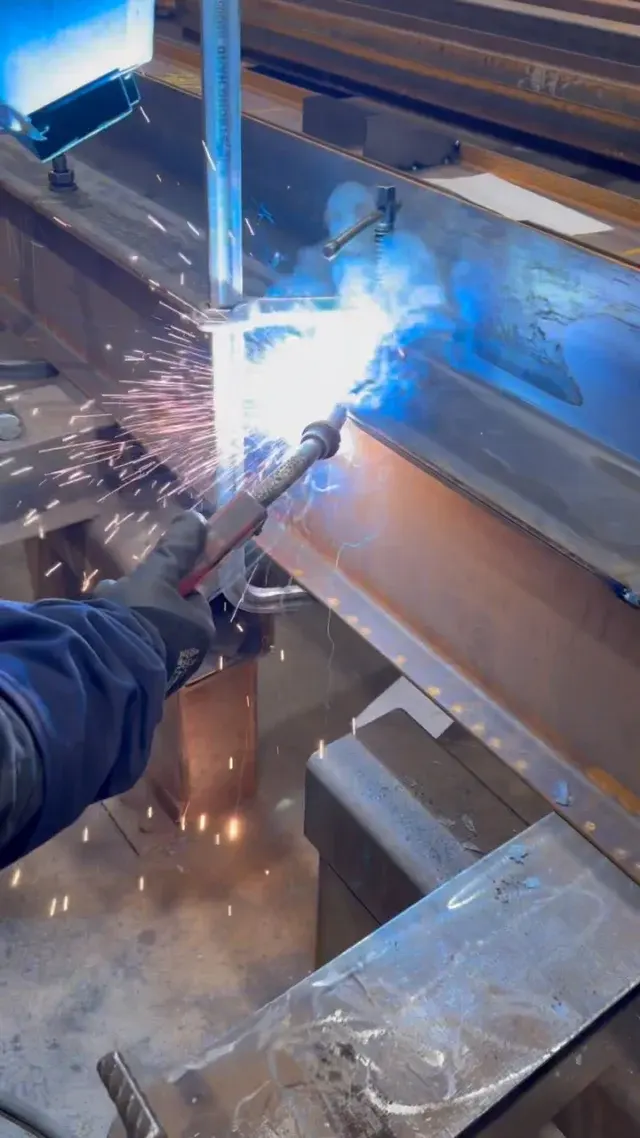
Welding
- Weld type, size and length match the welding symbols
- Visual inspection of every weld for cracks, porosity, undercut, incomplete fusion, overlap and profile
- Preheat applied where the procedure requires it
- NDT performed on the welds and at the frequency the specification calls for
- Repairs made to an approved procedure and re-inspected
Weld discontinuities and how they're judged are covered in structural weld defects and inspection.
Dimensions
- Overall length, straightness, sweep and camber within the tolerances of CSA S16 or the specification
- Connection-to-connection dimensions checked on columns and built-up members
Our guide to steel fabrication tolerances explains how those tolerances work.
Checklist: coating, marking and shipping
- Surface preparation done to the specified standard before priming or painting
- Primer or paint system as specified, and dry film thickness checked where required
- Areas to be left bare kept clean: faying surfaces of slip-critical joints, field weld zones, surfaces to be fireproofed if the fireproofing requires it
- Piece marks legible and matching the erection drawings
- Loose parts (bolts, clips, shims) bagged and tagged
- Steel loaded and blocked to prevent damage in transit
Checklist: erection
Field work has its own checks, and the erector's quality control and the general contractor share them.
- Anchor rods surveyed for position, projection and elevation before steel arrives
- Bearing surfaces, shims and grout as detailed (see grouting base plates)
- Members set in the right location and orientation, by piece mark
- Columns plumb and beams level within erection tolerances
- Temporary bracing in place until the permanent structure is stable
- Bolts installed to the right grade, length and tightness; pretension verified where specified
- Field welds made by a certified erector and inspected
- Touch-up of damaged coatings and field welds
- Deficiencies recorded, corrected and signed off
When something doesn't pass
A failed check is not a crisis if it's handled in order. The piece or connection is tagged and recorded as a nonconformance, the cause is identified, and the fix is agreed: rework to the drawings, a repair to an approved procedure, or, where the item can't meet the drawings, a disposition from the engineer of record. The repaired item is then re-inspected and the record closed. What causes trouble is the quiet fix that never makes it into the file, because the next reviewer has no way to know it happened.
Inspection reports and the QC file
An inspection report is only useful if someone else can follow it. A good one includes:
- project, drawing numbers and revision,
- the pieces, connections or welds inspected, by mark,
- what was checked, the method (visual, measurement, UT, MT and so on) and the acceptance standard,
- results, nonconformances and their resolution,
- the inspector's name, certification and date.
Ask at the start of the job which documents the owner, engineer and building department will want at the end. Mill certificates, welding procedures, welder qualifications and inspection reports are much easier to collect as the work happens than after the steel is enclosed.
Testing beyond inspection
"Structural steel testing" usually means non-destructive testing of welds, bolt tension verification, or coating thickness measurement. Additional material testing is rare when mill certificates are in order, but an engineer may ask for it with unidentified or salvaged steel, or for existing buildings where the original grade is unknown.
Quality built in at the shop
We fabricate to shop drawings prepared in-house, with shop welding certified by the Canadian Welding Bureau. Every piece leaves the shop cut, fitted, welded and marked to match the drawings. If your specification calls for third-party inspection, mill certificates or particular hold points, send it with your drawings and we'll confirm how we'll meet it in our quote.
Request a quote with your drawings and specification, or see our fabrication and welding services.
Frequently asked questions
Who inspects structural steel in Ontario?
Several parties: the fabricator's own quality control, a third-party inspection company when the specification requires one, the engineer doing general review of construction where the building code requires it, and the municipal building inspector.
Is third-party inspection required for structural steel?
Not on every job. CSA S16 requires the fabricator to control quality; third-party inspection is added by the project specification. S16 includes an informative annex that engineers can adopt to set an inspection class and frequency.
What does a structural steel inspection report include?
Typically the project and drawing references, the pieces or connections inspected, what was checked (material, dimensions, welds, bolts, coatings), the method used, the results, any nonconformances and how they were resolved, and the inspector's name and certification.
Who can inspect structural welds in Canada?
Welding inspectors are certified to CSA W178.2 through the CWB Group, at Levels 1 to 3, and inspection companies can be certified to CSA W178.1. Non-destructive testing is done by certified NDT technicians.