Yes, you can weld C-channel. Hot-rolled structural channel (C and MC shapes in grades like 350W or A36) is an ordinary weldable carbon steel, and fabricators weld it every day for frames, lintels, headers, bracing and supports. What makes a channel connection work is not whether it can be welded but how the joint is detailed: where splices go, how the channel is attached to what supports it, and how to keep a single channel from twisting under load.
This post covers the common ways channels are joined, spliced and connected, and what to put on the drawings. If you are new to the section itself, start with what C-channel steel is.
Welding C-channel: what changes compared with a beam
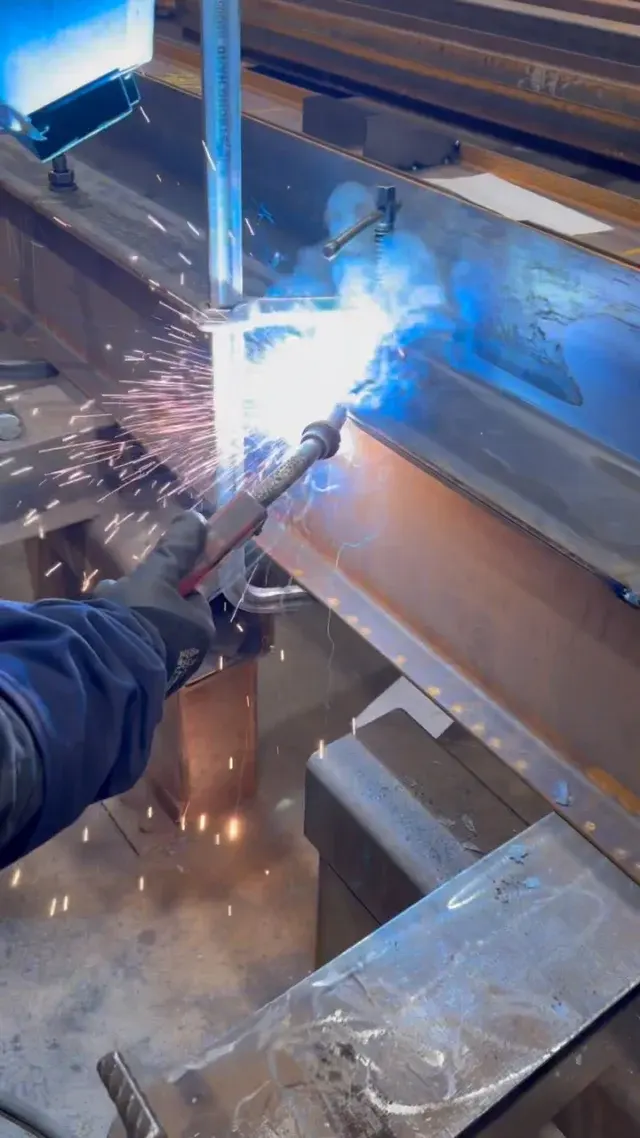
Channel is welded with the same processes and to the same standard as other structural shapes. In Canada that means CSA W59 for the welds, done by a company certified by the Canadian Welding Bureau. Our post on CSA W59 explains how that requirement comes through CSA S16 and the building code.
A few things are specific to channels:
- It is not symmetric. A C-channel has flanges on one side of the web only. Welding along one side pulls the piece toward that side as the weld cools, so long welds are sequenced and sometimes clamped to control distortion.
- The shear centre sits outside the web. A load applied through the web or flange tends to twist a single channel. Connections and bracing are detailed to resist that twist, which is why single channels used as beams need care. See can C-channel be used as a beam.
- Flanges are tapered. Standard C shapes have sloped inner flange faces. That affects bolting (bevelled washers) and the fit of plates welded inside the flanges.
- Thin toes heat quickly. On smaller channels the flange toes are thin, so heat input and weld size need to suit the material to avoid burn-through or undercut.
- Light-gauge "C" is a different product. Cold-formed C-studs, purlins and strut channel are thin, often galvanized, and are usually connected with screws, bolts or the manufacturer's fittings rather than structural welds. Our C-channel vs Unistrut post explains the difference.
Welding galvanized channel is possible, but the coating is removed at the weld area first and the weld is touched up afterwards. Where we can, we fabricate first and then prime or galvanize the finished piece.
Splicing C-channel lengths
"How to joint C-channel" usually means joining two lengths end to end. There are two main approaches:
| Splice type | How it works | Where it fits |
|---|---|---|
| Bolted splice plates | Plates on the web and often on the flanges, bolted to both channels across the joint | Field splices, lengths too long to ship, where welding on site is not wanted |
| Welded splice | Ends prepared and groove welded across the web and flanges, sometimes with added cover plates | Shop splices where the member must act as one continuous length |
Points to settle before anyone cuts steel:
- The engineer locates the splice. A splice belongs where bending and shear are low, not at midspan of a beam or over a support where the member is working hardest.
- Full strength or not. A splice may be designed to develop the full channel or only the forces at that point. The drawings should say which.
- Shop or field. Shop splices are easier to weld and inspect. Field splices are usually bolted because of the cost of field welding.
Ordering a member in one length avoids a splice altogether, within the limits of transport and handling. Our post on standard steel beam lengths and delivery limits covers what is practical to ship.
Connecting channel to columns, beams and walls
Channels are usually framed into other members the same way beams are, scaled down. The usual steel channel connection details:
- Shear tab. A plate welded to the column or supporting beam, bolted through the channel web. Simple and common for secondary framing.
- Clip angles. One or two angles bolted or welded to the channel web and to the support. Our post on clip angles and ledger angles covers these in detail.
- End plate. A plate welded across the channel end and bolted to the support face.
- Seat or bearing. The channel sits on a seat angle, a bracket, a wall or a pier, with a bearing plate if needed.
- To concrete or masonry. Anchors through the channel web into the wall, or a weld to an embed plate cast into the concrete.
For framing between two channels at a corner (a rectangular frame, a platform edge or a trailer frame), the ends are either coped and fitted so one channel frames into the web of the other, or mitred and welded around the profile. Mitred corners look clean but take more fitting and welding. Coped corners are easier to bolt.
Bolting through the flange needs a bevelled washer on the sloped inside face so the bolt head or nut bears flat. Bolting through the web needs no special washer.
Back-to-back, toe-to-toe and built-up channels
Two channels are often joined to act as one member:
- Back to back. The webs face each other with a gap, tied together with stitch plates or fillers at intervals. This makes a symmetric member, avoids the twisting problem of a single channel, and leaves a slot between the webs for gusset plates. Common for brace members, posts and headers.
- Toe to toe (boxed). The flange toes are brought together and welded along both seams, or joined with plates, to form a closed box. This gives good torsional stiffness, similar in behaviour to a tube.
- Channel with plate. A cover plate welded to the flanges, or a channel welded onto a W-beam flange, is sometimes used to strengthen a section or form a crane runway cap. These are design details for the engineer, not field improvisation.
The spacing of stitch plates or the weld pattern along a built-up member is part of the design. Too few ties and the two pieces act separately.
Joint plates, gussets and brackets
A "C-channel joint plate" can mean several things:
- Splice plate across an end-to-end joint.
- Gusset plate where braces meet, often bolted between back-to-back channels.
- Stitch plate or filler between built-up channels.
- Bracket or knife plate that connects a channel to a column or wall.
Each plate has a thickness, grade, bolt pattern and weld size that come from the connection design. On the shop drawings, every plate is detailed with its holes, edge distances and welds so it can be cut and fitted in the shop. For how connection plates are specified and ordered, see our post on steel plate cut to size.
What to send for a channel connection quote
Channel work is quick to fabricate when the drawings are complete. Useful information to send:
- channel size and grade (for example C200x17, 350W), and whether C or MC; our post on C vs MC channel explains the difference
- lengths and quantities, with any splice locations shown by the engineer
- the connection at each end: shear tab, clip angles, end plate, seat or anchors
- hole sizes and patterns, and any slots for adjustment
- weld sizes and whether welds are shop or field
- finish: bare, primed or galvanized
Structural connections must be designed by an engineer. If your drawings show the member but not the connection, ask us about our engineering services before fabrication.
Have your channels cut, welded and finished
We cut, drill, weld and mark C-channels to your drawings, with CWB certified shop welding, and can prime or galvanize to suit the job. Send your drawings through our quote request, or browse our steel products, including channels, plates and posts.
Frequently asked questions
Can you weld C-channel?
Yes. Hot-rolled structural channel in grades such as CSA G40.21 350W or ASTM A36 is a weldable carbon steel. For structural work in Canada the welding should be done to CSA W59 by a company certified by the CWB.
How do you join two lengths of C-channel?
With a splice: either bolted splice plates on the web and flanges, or a groove weld across the full section, sometimes with added plates. Where the splice goes and how it is made should be designed by the engineer, because a splice in the wrong place can weaken a member.
What is a C-channel joint plate?
A plate that joins channels to each other or to another member: a splice plate across a joint, a gusset plate at a brace, or a stitch plate tying two channels back to back. Its size, thickness, bolts and welds come from the connection design.
Can you bolt through the flange of a C-channel?
Yes, but standard C-channels have sloped inner flange faces, so a bevelled (tapered) washer is normally used under the nut or bolt head on the inside of the flange so it bears flat.