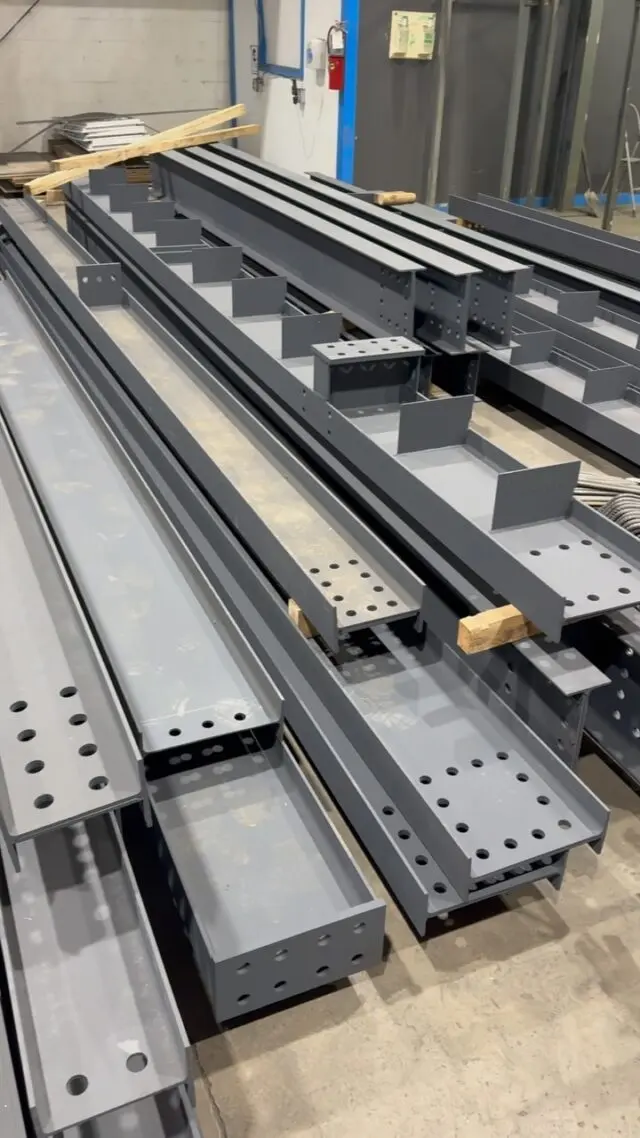
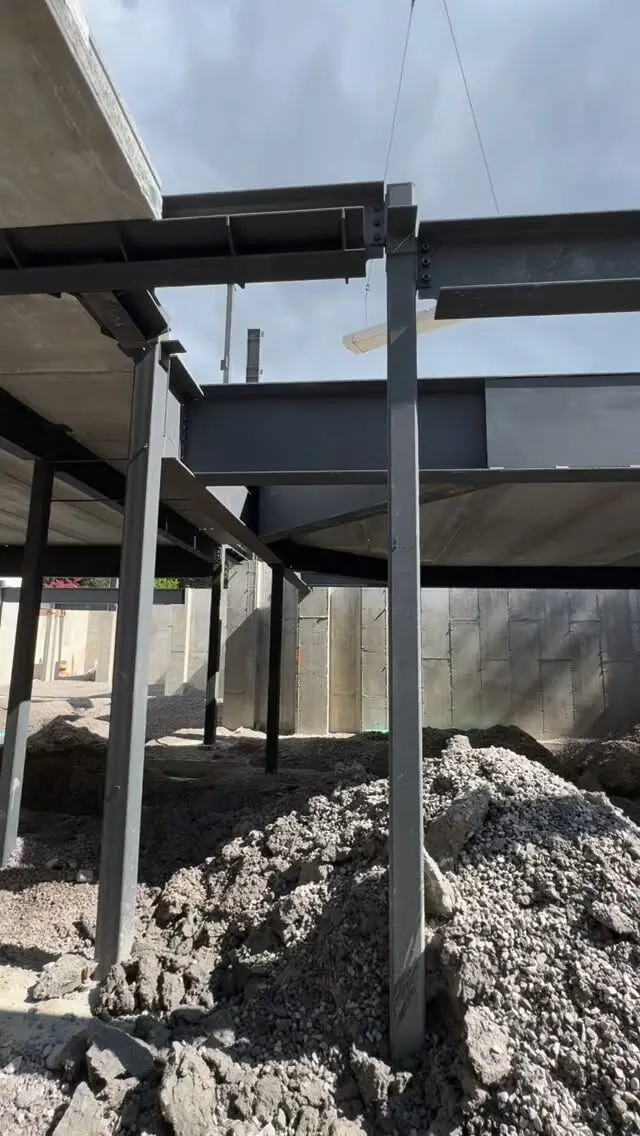
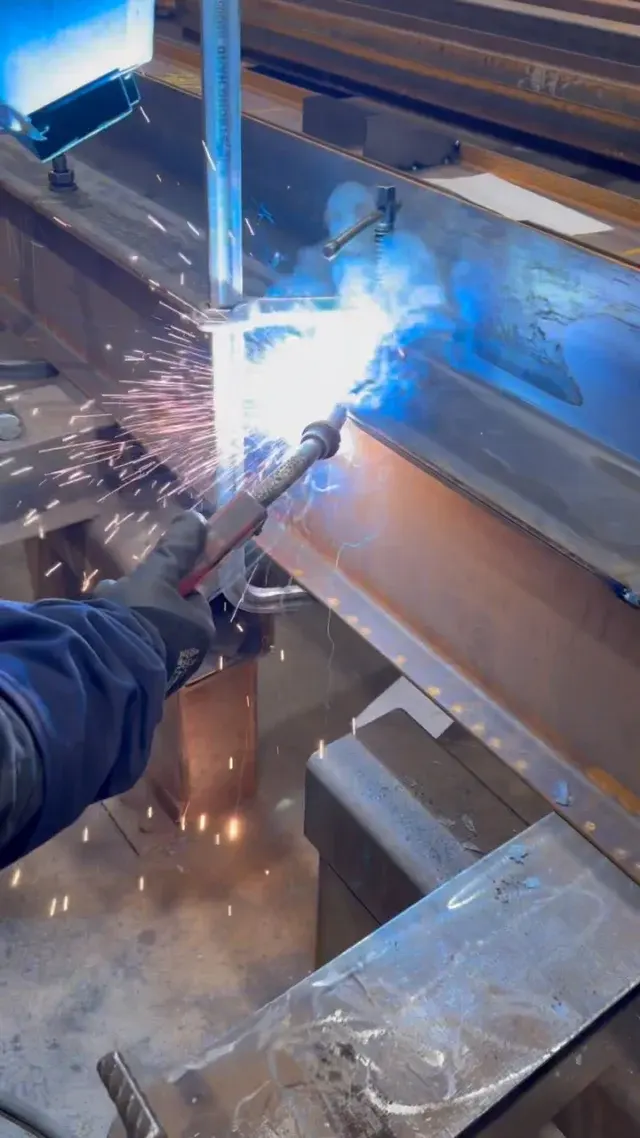
There are two ways to camber a steel beam. Cold cambering bends the beam in a hydraulic cambering machine and is the faster, more common method for standard beams. Heat cambering uses a torch to heat wedge-shaped zones that shrink as they cool and pull the beam into a curve; it is slower but works on beams a machine can't handle, such as short, very deep or built-up members, and it can fine-tune or correct camber. Both produce a usable beam when done properly, and the engineer, not the method, decides how much camber is needed.
What camber is and why beams get it
Every beam sags a little under load. Camber is a gentle upward curve built into the beam before it's installed, so that when the dead load of the floor or roof goes on, the beam settles closer to level. Benefits include:
- Flatter floors and roofs, with less concrete needed to level a sagging deck.
- Less ponding on flat roofs.
- In some designs, a lighter beam than would be needed to meet the deflection limit without camber.
Camber is shown on the structural drawings, usually as a dimension at midspan (for example "camber 25 mm"). Beams also come from the mill with a small amount of natural, uncontrolled camber from rolling and straightening. That mill camber is not the same as specified camber, which is induced deliberately, either at the mill or in the fabricating shop.
Cold cambering: how a beam cambering machine works
A beam cambering machine is a rigid frame with hydraulic rams. The beam is held at two support points near its ends while the rams push on it at two load points closer to the centre. That loading pattern produces a curve close to the shape the beam will deflect into under a uniform load.
The operator pushes the beam well past the target curve, holds it briefly, then releases. The beam springs back, but the outer fibres have yielded, so a permanent curve remains. If there isn't enough camber, the rams go again. It is quick: a standard beam can be cambered in minutes.
Strengths of cold cambering:
- Fast and repeatable for long runs of similar beams.
- Little effect on the steel's properties. An AISC Engineering Journal paper on cambering notes that cold-cambered beams can be designed with the same allowable stresses as uncambered ones once the steel has rested for a few hours.
Limits of cold cambering:
- Length. The machine supports the beam a fixed distance apart and needs some beam beyond each support. Published rules of thumb, including an AISC Engineering Journal paper on cambering, put the shortest beam that can practically be cold cambered at roughly 6 to 7 m (20 to 24 ft).
- Depth and weight. Each machine has a maximum (and minimum) section it can bend. Shallow beams are hard to camber accurately, and the heaviest, deepest sections can exceed a machine's capacity.
- Small cambers. The same sources suggest not specifying camber below roughly 20 to 25 mm (3/4 to 1 in), because part of a small camber is lost and the result is unreliable.
- Over-cambering. If a beam goes too far, it must not be forced back the other way in the machine. Reversing cold bending can weaken the steel. The fix is controlled heat, which is one reason shops that cold camber also need heat-cambering skills.
Heat cambering: how it works
Heat cambering uses the fact that steel expands when heated and, if restrained, shortens permanently as it cools. The fabricator heats a wedge-shaped (V-shaped) area of the web with the wide end of the V running across the flange that will be on the inside of the curve. The surrounding cooler steel restrains the hot zone, so when it cools it is a little shorter than before. Several of these wedges, placed symmetrically along the beam, add up to a smooth camber.
A few features of the process:
- Temperature is controlled. The AISC Specification for Structural Steel Buildings limits heated areas to 650 °C (1,200 °F) for most structural steels and 590 °C (1,100 °F) for quenched-and-tempered grades. Fabricators monitor temperature with temperature-indicating crayons or instruments. AISC notes that temperatures above about 700 °C (1,300 °F) can change the properties of some steels, which is exactly what the limits are there to prevent. On Canadian projects, the requirements of CSA S16 and the project specification govern, so confirm the limit your specification sets.
- The beam moves the wrong way first. During heating, the beam bows away from the intended camber. It reverses as it cools, which is why the operator works to a plan rather than by eye.
- Cooling is slow and natural. Best results come from letting the beam cool on its own.
- It's skilled work. Wedge size, angle, spacing and number all affect how much the beam moves. It takes experience and measurement to hit a target camber.
Strengths of heat cambering:
- No minimum length set by a machine, so short beams can be cambered.
- No upper size limit from ram capacity, so deep or heavy beams and built-up girders can be cambered.
- Works about either axis, so it can also add or remove sweep (sideways curve) and straighten bent members.
- Can be applied to channels, angles and HSS as well as wide-flange beams.
- Can correct over-camber, or add camber locally.
Limits of heat cambering:
- Slower and more labour-intensive than a machine, especially for many identical beams.
- Requires trained operators and temperature control.
- Best suited to ordinary carbon structural steels; special high-strength or heat-treated grades need extra care or may be excluded by the specification.
Heat vs cold cambering compared
| Cold cambering | Heat cambering | |
|---|---|---|
| How | Hydraulic rams bend the beam past its yield point | Wedge-shaped heats shrink one side as they cool |
| Speed | Fast, minutes per beam | Slower, depends on size and camber |
| Short beams | Limited by machine support spacing | Possible |
| Deep or heavy beams | Limited by machine capacity | Possible |
| Sideways curve (sweep) | Not usually | Yes |
| Correcting over-camber | Not by reverse bending; uses heat | Yes |
| Key control | Ram travel and spring-back | Temperature and heat pattern |
Many shops use both: cold cambering for long runs of standard beams, heat for everything else.
Which beams should and shouldn't be cambered
Engineering literature on cambering, including the AISC Engineering Journal, lists types of members that generally don't suit camber. The usual list includes:
- Beams with cantilevered ends.
- Beams with moment connections at the ends.
- Crane beams and girders.
- Spandrel beams carrying cladding, where camber makes the facade harder to align.
- Members with non-uniform cross sections or partial-length cover plates.
- Short or shallow beams, and beams that would need only a very small camber.
Good candidates are long, simply supported floor and roof beams of uniform section, especially composite floor beams where wet concrete adds a lot of dead load.
This is the engineer's decision. If you think a beam needs camber that isn't on the drawings, or a beam is cambered and you're not sure why, raise it with the engineer of record rather than adding or removing it in the field.
Specifying and checking camber
A few practical points help camber go smoothly:
- Show the amount and direction on the drawings for each cambered beam, and say what load it is meant to offset.
- Leave the method to the fabricator unless there's a reason not to. Specifications sometimes restrict the method; if yours does, the fabricator needs to know at the quote stage.
- Camber is checked in the shop. Once a beam is erected, connected and loaded, its own weight and the end restraint make camber hard to measure reliably.
- Cambering usually comes after cutting and drilling. Beams that need square, parallel ends for end plates are often cut after cambering. Your fabricator's shop drawings will show the sequence.
- Expect some variation. Camber is not a precise science, and actual deflection rarely matches the calculation exactly. Tolerances come from the governing standard and the project specification.
Cambered beams from our shop
We fabricate wide-flange beams with connections and camber as specified, and heat cambering of beams is one of the specialty services we offer. If your drawings call for cambered beams, include the camber notes when you send them and we'll tell you how we'd handle them in the quote. If you're still choosing who will fabricate your steel, our guide on choosing a structural steel fabricator in Ontario covers what to ask, and our W-shape beam chart lists common beam sizes.
Send us your drawings for a quote, or read more about our fabrication services.
Frequently asked questions
What is camber on a steel beam?
Camber is a slight upward curve built into a beam so that, once the floor or roof load is applied and the beam deflects, it ends up closer to level. The amount is set by the structural engineer and shown on the drawings.
How do you camber a steel beam with heat?
A trained fabricator heats wedge-shaped zones of the web and one flange with a torch, keeping the steel below a set temperature limit. As the heated zones cool, they shrink and pull the beam into a curve. The temperature limit and procedure come from the governing standard and specification.
What is a beam cambering machine?
It is a heavy frame with hydraulic rams that bends a beam cold. The beam is supported near its ends, the rams push it past the target curve and it springs back to a permanent camber. Each machine has a range of beam sizes and lengths it can handle.
When should steel beams be cambered?
Camber is usually considered for long, simply supported floor or roof beams where dead-load deflection would otherwise leave a visible sag or ponding. Short, shallow, cantilevered and moment-connected beams are generally poor candidates. The engineer makes the call.