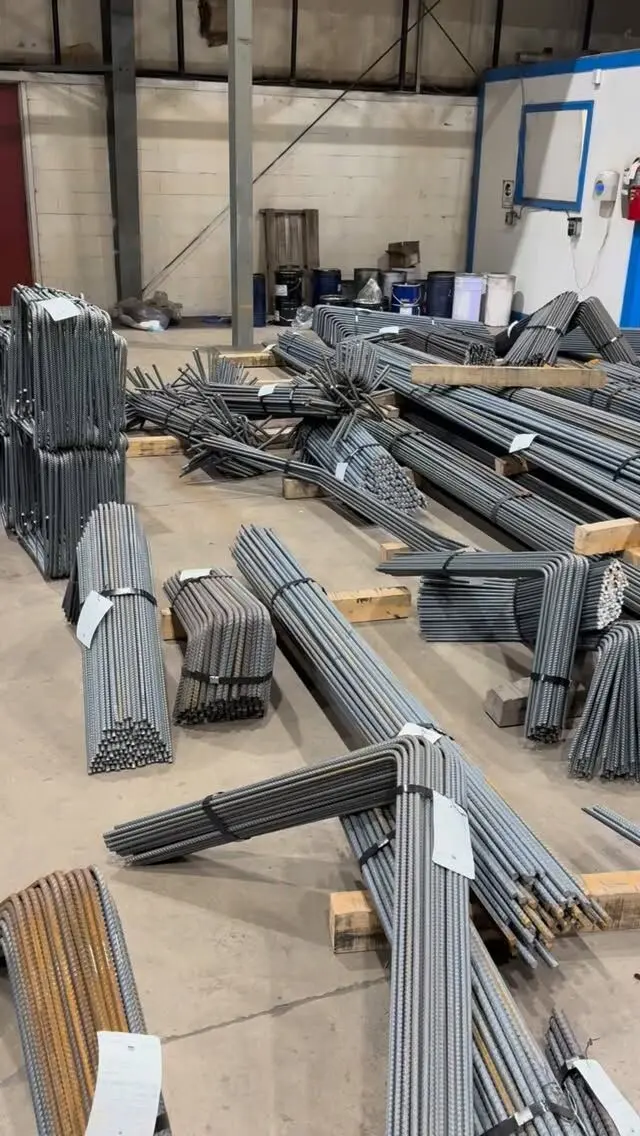
A bar bending schedule (BBS) is a table that lists every reinforcing bar in a concrete element: its bar mark, size, number of pieces, cut length, bent shape and the dimension of each leg. The shop cuts and bends from it, and the crew on site uses the bar marks to put each bar in the right place. In Canada the same document is normally called a bar list, and it follows the Reinforcing Steel Institute of Canada (RSIC) format rather than the British shape codes many online templates use.
This guide explains what a bar bending schedule contains, how to read one line by line, how the international BBS maps onto a Canadian bar list, and where spreadsheets and calculators help or fall short.
What a bar bending schedule does
A structural drawing tells you what the concrete needs: 15M bars at 300 mm each way in the footing, 4-20M top and bottom in a beam, ties at a set spacing in a column. It does not tell a shear operator how long to cut each bar or how far apart to put the bends. The bar bending schedule turns the design into a cutting and bending list.
It does three jobs at once:
- Fabrication. Every line gives the shop exactly what to shear and bend, so nothing is guessed on the shop floor.
- Identification. Each line has a bar mark that also appears on the placing drawing and on the bundle tag, linking the bar on the ground back to its spot in the structure.
- Quantity and weight. Summing the lines gives the total length and mass of each bar size. Rebar is sold on its theoretical mass, so the schedule is also the basis for quantities on the order.
The RSIC Manual of Standard Practice describes the bar list in the same way: it lets the fabricator make the bars in the right length and shape, and it identifies the finished material for use in the field.
How to read a bar bending schedule, column by column
Formats vary between countries and software, but almost every bar bending schedule carries the same information. Here is a simplified Canadian-style bar list with three typical lines (the values are illustrative):
| Item | Bar mark | Total | Size | Length (mm) | Type | A | B | C | Remarks |
|---|---|---|---|---|---|---|---|---|---|
| 1 | F101 | 24 | 15M | 2 400 | straight | Footing F1, bottom, short way | |||
| 2 | W203 | 40 | 15M | 1 920 | 17 | 600 | 800 | 600 | Wall W2, top of wall U-bars |
| 3 | C305 | 18 | 10M | 1 560 | T1 | Column C3 ties, see sketch |
Reading across a line:
- Item is just the line number on the sheet.
- Bar mark is the unique label for that size, length and shape. If two bars differ by a single leg dimension, they get different marks.
- Quantity. The RSIC sample bar list has a "per band" column next to the total, used when a group of bars repeats; the total is what the shop makes.
- Size is the Canadian metric bar designation, 10M to 55M.
- Length is the total length of bar the shop shears before bending. For a straight bar it is simply the bar length.
- Type is the bend shape from the RSIC typical bar bends table, such as 17 for a square-cornered U-bar or T1 for a closed column tie. Shapes not in the table are type X with a sketch.
- A, B, C... are the leg dimensions for that type, in the order shown on the type's sketch.
- Remarks carry location, grade if it varies, coating and anything critical.
The header matters as much as the lines. The RSIC sample sheet carries the project, contract, structure, grade, drawing number, revision, date and who prepared it. Always check that the drawing and revision on the schedule match the drawings you are building from.
Leg dimensions and cut length are not the same thing
The most common reading mistake is adding the legs and expecting the total to match the length column. Under RSIC practice, leg dimensions are out-to-out of the bar, measured to the outside of each bend, except the A and G dimensions on standard 135° and 180° hooks. Because the bar cuts the corner around each bend, the length the shop shears is a little shorter than the out-to-out legs added together. How much shorter depends on the bar size, the bend diameter and the bend angle.
In the example above, the U-bar's legs add to 2 000 mm while the cut length is 1 920 mm. That gap is not an error. Detailing software and the fabricator's bending tables work it out for each size. Our rebar bending chart lists the bend diameters behind it.
Working out the weight
Weight comes straight from the schedule: total length of a size multiplied by its mass per metre. Using the nominal mass of 15M bar (1.570 kg/m under CSA G30.18), line 1 above is 24 bars at 2.4 m, or 57.6 m, which is about 90 kg. RSIC practice is to list the total mass for each bar size separately. Our rebar weight chart has the mass per metre for every size.
Bar bending schedule vs the Canadian bar list
If you have worked in the UK, India, the Middle East or Australia, or you downloaded a BBS template online, the layout will look different from what a Canadian shop sends you. The underlying idea is identical; the conventions are not.
| International BBS (BS 8666 style) | Canadian bar list (RSIC) | |
|---|---|---|
| Name | Bar bending schedule, BBS | Bar list, bar schedule, sometimes "rebar bending list" |
| Bar sizes | Nominal diameters in mm with a type letter | 10M to 55M to CSA G30.18 |
| Shapes | Two-digit BS 8666 shape codes | RSIC typical bends: numbered types, S stirrups, T ties, type X |
| Quantity | Often number of members times bars in each | Total quantity, with a per-band column on the RSIC form |
| Leg dimensions | Defined by each shape code's rules | Out-to-out, except standard hook A and G |
| Governing practice | BS 8666 and the local code | RSIC Manual of Standard Practice, CSA A23.1 and A23.3 |
The two sets of shape codes are not interchangeable. A "shape code 21" on a British schedule and a "Type 21" in the RSIC table are not the same bar (RSIC does not use 21 at all). If your schedule came from an overseas consultant or template, have it converted to RSIC bend types before it goes to a Canadian fabricator. Our guide to rebar bending shape codes lays out the RSIC types and how they differ from other systems.
Types of bar bending schedule
People searching for "types of bar bending schedule" usually mean one of two things.
Schedules by structural element. Most bar lists are split by part of the structure, because that is how the concrete gets poured and how the steel gets delivered:
- Footings and pile caps: mostly straight bars, dowels and some hooked bars.
- Foundation and retaining walls: verticals, horizontals, corner bars and U-bars at openings and ends.
- Columns: verticals (often offset-bent at splices) and ties.
- Beams: top and bottom bars, extra bars over supports, and stirrups.
- Slabs: bottom and top mats, edge bars, and support bars.
- Stairs and ramps: bent bars that follow the profile.
Schedules by stage. An estimating schedule counts enough to price the job. A fabrication schedule is the detailed, checked list the shop cuts from, tied to the placing drawings and released by pour or by area. They are not the same document, and a quick take-off should never go to the shear. Our guide to placing drawings vs bar lists explains how the fabrication schedule and its drawings work together.
Bar bending schedules in Excel and calculators
Spreadsheets and online BBS calculators are popular, and they have a place:
- Good for: estimating quantities and weights, checking a supplier's tonnage, planning how much bar a pour needs, and ordering a handful of straight bars or simple dowels.
- Not reliable for: final cut lengths of bent bars. Many free calculators use bend deduction rules from other countries' standards, which do not match Canadian bend diameters or RSIC out-to-out dimensioning. They also do not know about laps, cover, openings and site conditions unless you put them in correctly.
If you do build your own list, use the RSIC columns (mark, quantity, size, length, type, legs, remarks), give every leg dimension, and state the grade and any coating. RSIC practice is to give bar lengths to the nearest 20 mm, with a note where a dimension is critical. Then let your fabricator check it before fabrication. A shop will build exactly what the paper says, which is good news when the paper is right and expensive when it is not.
For the ordering side, including tags, delivery and checking a load, see how to order cut and bend rebar.
Common mistakes on a bar bending schedule
Most problems trace back to a few habits:
- Wrong revision. The schedule was prepared from drawings that have since changed.
- Missing laps. Lap length is the engineer's call. If the drawings are silent, ask before the list is finalized.
- Cover not deducted. Bar lengths have to fit inside the concrete with the specified cover at each face.
- Duplicate marks. Two different bars with the same mark will end up swapped on site.
- Foreign shape codes. A BS 8666 code sent to a Canadian shop leaves the shop to guess.
- Grade left off. If a job needs 500W or a mix of grades, the schedule has to say where.
Getting a bar list prepared for your project
You do not need to produce a bar bending schedule yourself to order fabricated rebar. Send us your structural drawings and we prepare a free take-off and quote, then the bar lists and placing drawings once the work is approved. We cut, bend, tag and bundle 10M to 55M bar in our shop and deliver across the GTA and Ontario.
Send your drawings for a quote, or see our detailing, cut and bend and delivery services.
Frequently asked questions
What is a bar bending schedule?
A bar bending schedule (BBS) is a table that lists every reinforcing bar in a concrete element by bar mark, with its size, quantity, cut length, bent shape and the dimension of each leg. The fabricator cuts and bends from it, and the site crew uses the marks to place the bars.
Is a bar bending schedule the same as a bar list?
They do the same job. Bar bending schedule is the British and international term; in Canada the document is usually called a bar list, and it follows the format and bend types in the RSIC Manual of Standard Practice rather than BS 8666 shape codes.
Who prepares the bar bending schedule?
Usually the rebar detailer working for the fabricator, from the engineer's structural drawings. On many jobs the bar list and placing drawings are reviewed by the engineer or contractor before anything is cut.
Can I make a bar bending schedule in Excel?
A spreadsheet is fine for estimating quantities and weights, or for a simple order of straight bars and a few bends. For fabrication, the cut lengths and bend dimensions have to follow the fabricator's bending standards, so most shops prefer to detail the list themselves or check yours before cutting.
What are the types of bar bending schedule?
There is no formal set of types. The phrase usually means schedules organized by structural element (footings, columns, beams, slabs, walls, stairs), or schedules prepared at different stages, such as an estimating schedule for the quote and a fabrication schedule for the shop.