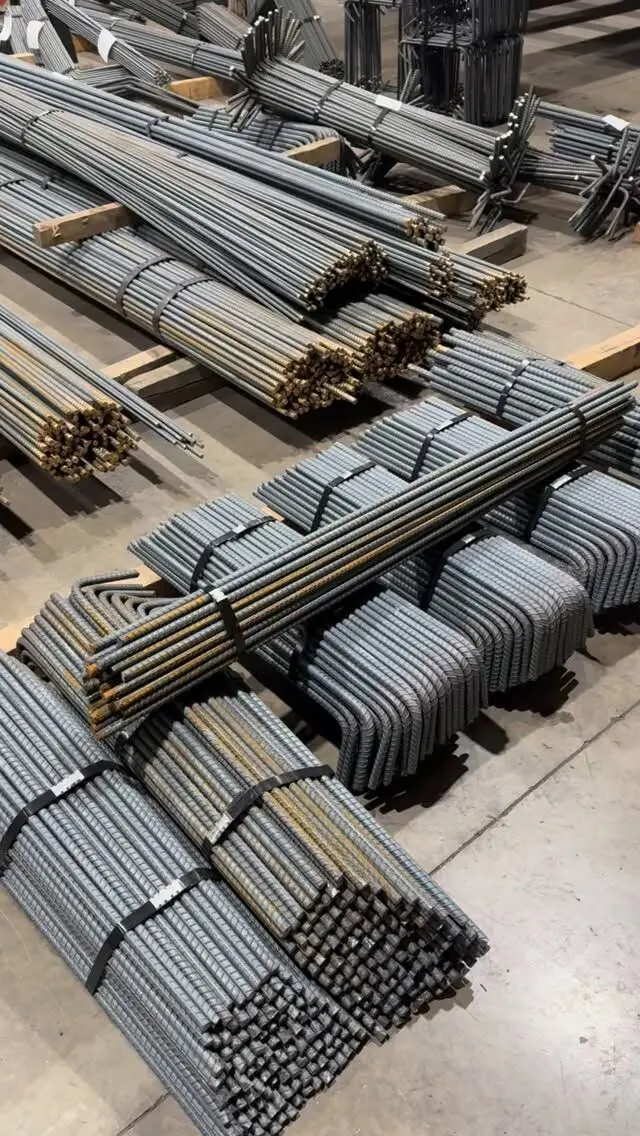
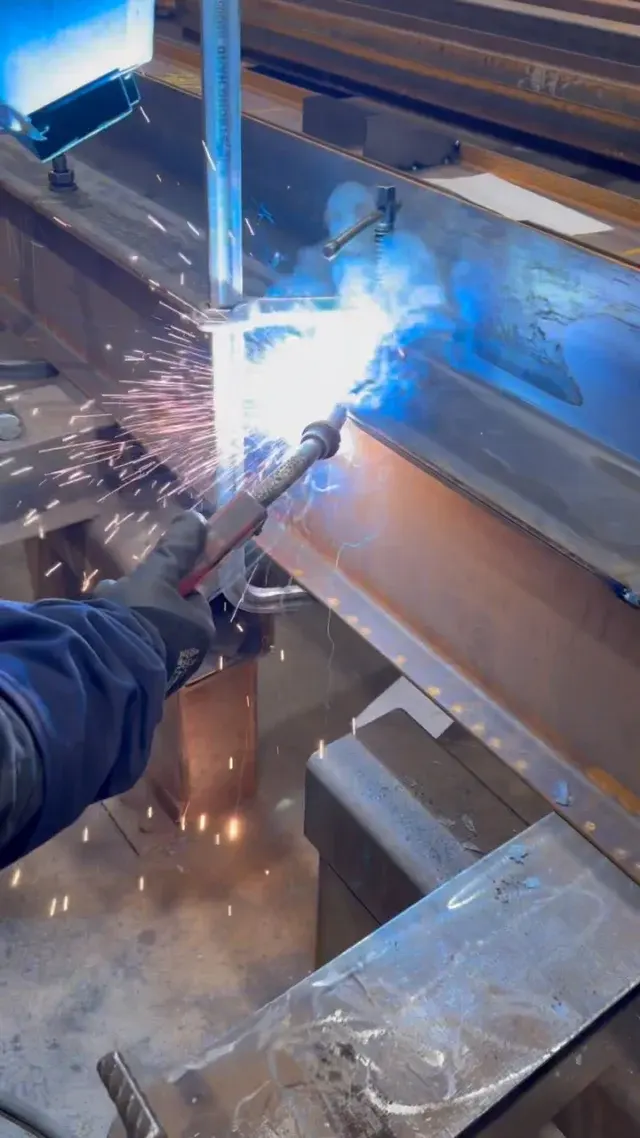
In Canada, weldable rebar is bar made to one of the "W" grades in CSA G30.18, most commonly 400W, with 500W used where higher strength is specified. The W grades have restricted chemistry, including a carbon equivalent limit, so the steel can be welded with a qualified procedure. Being weldable does not make welding automatic, though: CSA A23.1 requires welding of reinforcement, including tack welding, to follow CSA W186, and most bar on site is still tied, not welded.
This post explains what the grade letters mean, when welding rebar is allowed, why it is usually avoided and what to ask for if your drawings do call for it.
What the W in 400W means
CSA G30.18, "Carbon steel bars for concrete reinforcement", is the Canadian standard for deformed steel rebar. It defines grades by a number (the specified minimum yield strength in MPa) and a letter:
| Grade | Yield strength | Letter means | Typical use |
|---|---|---|---|
| 400R | 400 MPa | Regular grade | Bar where welding and enhanced ductility are not needed |
| 400W | 400 MPa | Weldable grade | The default on most Canadian drawings |
| 500R | 500 MPa | Regular grade | Higher-strength bar, no welding |
| 500W | 500 MPa | Weldable grade | Higher-strength bar where welding or ductility matters |
The W grades are intended for applications where welding, bending or ductility are a concern. Compared with R grades, they have tighter limits on chemistry and mechanical properties:
- Carbon equivalent. The W grades cap the carbon equivalent of the heat (a single number combining carbon, manganese and other alloying elements). For 400W in the 2009 edition of G30.18, the limit is 0.55%, as reproduced on mill specification sheets. A lower carbon equivalent means the steel is less prone to hardening and cracking next to a weld.
- Chemistry limits. Maximum carbon, manganese, phosphorus, sulphur and silicon are specified.
- A maximum yield strength. W grades have a ceiling as well as a floor on yield strength, which keeps bars from being much stronger than the designer assumed. That matters for ductile design in seismic regions.
Grade 400W is what most Canadian structural drawings call for, so in practice most bar you buy in Ontario is already a weldable grade. Our post on rebar grades in Canada covers 400W and 500W in more detail, and types of rebar in Canada puts them alongside coated bar and GFRP.
To confirm what you have, look at the mill test certificate for the heat number on the bundle tag. It shows the grade and the chemistry, including the carbon equivalent.
What the standards say about welding rebar
Three CSA standards work together:
- CSA A23.1 (concrete materials and construction) requires that welding of reinforcement conform to CSA W186, and that tack welding of reinforcing bars also be done to CSA W186. It also covers welding of steel hardware (embed plates and the like) under CSA W59, while welding reinforcing bars to that hardware falls back under W186.
- CSA W186, "Welding of reinforcing bars in reinforced concrete construction", covers certification of companies that fusion weld rebar, qualification of their personnel and procedures, and the design, fabrication and inspection of welded rebar connections. That includes bars welded directly to each other, through splice members, and to structural steel used as anchorage, in the shop or the field.
- CSA A23.3 (concrete design) recognises welded splices as one way to join bars, alongside lap splices and mechanical splices, with the strength requirement set by the designer.
W186 certification is administered by the Canadian Welding Bureau. A certified company has to qualify its welders and tack welders, have its welding procedures accepted, and employ qualified welding supervisors and engineering personnel. According to the CWB, there are two divisions: Division 1 companies have full-time engineers and Division 2 companies retain part-time engineers.
This is separate from CSA W47.1, which certifies companies welding structural steel. A shop certified to W47.1 for beams and columns is not automatically certified to weld rebar. If your drawings call for welded reinforcement, ask specifically for W186. Our post on why to hire a CWB certified fabricator explains how CWB certification works for structural steel.
Why most rebar is tied, not welded
Even with weldable bar, tying is the default for good reasons:
- Heat affects the bar. A weld heats a small zone of the bar to very high temperature and then lets it cool quickly. Next to the weld, the steel's structure changes and can become harder and more brittle, or softer and weaker, depending on the chemistry and how the bar was made.
- Heat-treated bar loses strength. Some bar gets its strength from controlled cooling at the mill rather than from alloying. Welding heat can undo that locally. This is one reason W186 procedures are specific to the bar and process.
- Tack welds make notches. A small, quick tack weld cools fastest of all and can leave a hard spot or tiny crack on the bar surface. Under repeated or seismic loading, that is where a bar can fail.
- It costs more. Welding needs certified welders, approved procedures, inspection and power on site. Tie wire needs a pair of pliers or a tying tool.
- It is rarely needed. Ties only have to hold bars in place until the concrete sets. The concrete does the structural work, not the tie.
That is why "can rebar be welded instead of tied?" has a short answer: not unless the engineer specifies it and the work is done to W186. Welding mats or cages together "to make them stiffer" without that approval is not acceptable, even with 400W bar.
When welding rebar makes sense
Welded rebar does have a place, usually decided at the design stage:
- Welded splices for large bars, where lap splices are not permitted (CSA A23.3 does not allow lap splices for bars larger than 35M except in limited compression cases) or where congestion leaves no room for laps.
- Bars welded to embed plates, anchors and steel members, such as rebar anchors on plates cast into walls for connections.
- Prefabricated cages and mats that are tack welded so they hold their shape when lifted, where the engineer accepts it and the shop is certified to W186.
- Precast concrete, where welded reinforcement and embedded connections are common.
For joining bars without welding, mechanical couplers are often simpler. Our comparison of rebar couplers vs lap splices covers when each is used.
Weld size and procedures
Searches for "rebar weld size" are usually looking for a rule of thumb, such as a flare-bevel or lap weld of a certain length per bar diameter. In Canada, weld sizes, lengths and joint types for rebar come from the engineer's design and the welding procedures accepted under CSA W186, not from a general table. W186 also covers how welds are inspected, including methods for butt joints between bars.
If your drawings show welded reinforcement, check that they give:
- The bar grade (a W grade) and size.
- The joint type and weld size or the strength the splice must develop.
- Any inspection or testing requirements.
- Whether the welding is done in the shop or in the field.
A quick checklist for welded rebar
- Specify a W grade on the drawings and bar list, and confirm it on the mill certificates.
- Use a W186 certified company for any welding of reinforcement, including tack welding.
- Do not weld near bends unless the design says so. Bent areas have already been worked and are more sensitive.
- Keep welding away from epoxy-coated bar unless the specification covers coating repair; heat destroys the coating.
- Get approval in writing before replacing tied or lapped details with welded ones.
Getting bar for welded details
Most of our rebar orders are tied in the field, but if your drawings include welded reinforcement, tell us when you send them so the bar grade and detailing are right from the start, and ask us about welded rebar assemblies for your job. We supply 10M to 55M bar detailed, cut, bent and tagged to your bar list. Send your drawings for a free take-off and quote, or see our rebar products.
Frequently asked questions
Which rebar is weldable?
In Canada, the weldable grades are the W grades in CSA G30.18, such as 400W and 500W. They have restricted chemistry, including a carbon equivalent limit, so they can be welded with a qualified procedure. R grades do not carry those limits.
Can rebar be welded instead of tied?
Only where the engineer allows it and the welding follows CSA W186. Tie wire is the normal way to hold bars in position. Welding, including tack welding, can damage the bar and is not a substitute for tying unless it is designed and done to the standard.
Why is rebar not welded?
Welding heats the bar locally and can make the steel next to the weld brittle or weaker, especially in higher-carbon bar or bar that gets its strength from heat treatment at the mill. Tying is faster, needs no certified welders and does not affect the bar.
Who can weld rebar in Canada?
CSA A23.1 sends welding of reinforcement to CSA W186, which certifies companies through the Canadian Welding Bureau and requires qualified welders, approved procedures and supervisory and engineering personnel.