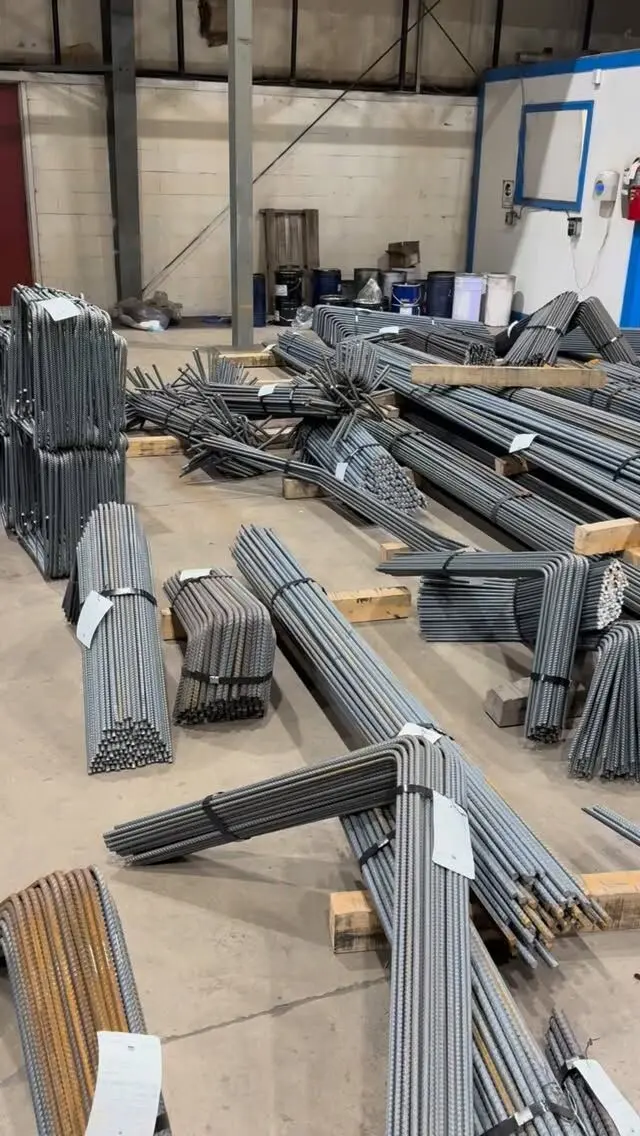
Rebar fabrication cost is the work that turns straight mill bar into the pieces on your bar list: cutting, bending, tagging and bundling, plus the detailing and handling around it. The biggest driver is not the tonnage but the number of pieces and bends in that tonnage. A tonne of long straight 25M is a couple of dozen cuts; a tonne of 10M stirrups is hundreds of pieces, each with several bends.
This guide explains how fabricators look at a bar list when they price it, why stirrups and dowels behave differently from straight bar, and what you can do to keep the cost down without cutting corners.
What rebar fabrication includes
When you order fabricated rebar, the price covers more than the steel:
- Detailing (if the fabricator is producing the bar list and placing drawings from your structural drawings).
- Cutting each bar to length, usually by shearing in the shop.
- Bending to shape on bending equipment, to the bend diameters and tolerances required by CSA A23.1 and the drawings.
- Tagging every bundle with the bar mark, size, quantity and shape.
- Bundling and loading by pour or by area, so the right steel comes off the truck at the right time.
- Delivery to site.
Material and fabrication may be shown as one rate or split. Either way, both parts are in the number. For the material side and what moves it, see what drives rebar prices in Canada.
Pieces per tonne: the hidden driver
Because rebar is sold by weight, it's easy to think of fabrication as a per-tonne cost. In the shop, the work is per piece and per bend. These examples show how much the piece count changes with size and shape (lengths are illustrative, not from any particular design):
| Example piece | Developed length | Weight per piece | Pieces per tonne |
|---|---|---|---|
| 25M straight bar | 12 m | about 47.1 kg | about 21 |
| 15M straight bar | 6 m | about 9.4 kg | about 106 |
| 15M L-shaped dowel | 1.2 m | about 1.9 kg | about 531 |
| 10M closed stirrup | 1.8 m | about 1.4 kg | about 708 |
| 10M tie | 1.2 m | about 0.9 kg | about 1,062 |
Developed length is the full length of bar in the piece, including hooks and bends, and it is what the weight is calculated on. The point of the table: a tonne of stirrups or ties can be fifty times as many pieces as a tonne of heavy straight bar, and every piece is cut, bent, counted and tagged. That is why a bar list heavy in small fabricated pieces costs more per tonne to fabricate.
What makes a bar list more or less expensive to fabricate
Number of bar marks. Every distinct mark is a separate setup, a separate tag and a separate bundle. A design with many near-identical marks that differ by a few millimetres takes longer than one with fewer, standardised marks.
Shape complexity. A straight cut is the simplest operation. A single 90-degree hook adds a bend. Stirrups and closed ties have several bends. Spirals, hoops, multi-plane bends and custom radii take longer again, and some need special equipment.
Bar size. Small bars mean more pieces per tonne. Large bars are fewer pieces but heavier to handle and need larger bend diameters.
Tolerances and special requirements. Tight tolerances, mechanical splices, threaded ends or specific bend diameters beyond the standard all add work.
Coated bar. Epoxy-coated bar has to be cut and bent without damaging the coating, and damaged areas need repair. Galvanized and stainless bar have their own handling requirements. Coated work is usually priced differently from plain bar.
Revisions. Changes after the bar list is released can mean re-detailing, re-cutting or scrapping bent pieces that no longer fit. Late revisions are one of the most avoidable fabrication costs.
Schedule and phasing. Splitting an order into many small releases means more setups and more deliveries. Phasing that follows the pour sequence is worth it; very small, frequent releases add cost.
Delivery. Distance, access and the number of drops. Small orders carry delivery as a bigger share of the total.
Stirrups and dowels
Stirrups and dowels are the items people most often ask about individually, because they show up on almost every job.
Stirrups and ties wrap around the main bars in beams, columns and grade beams. They are short, light and multi-bend, so they sit at the high end of the per-tonne fabrication cost. Ordering them fabricated almost always makes sense, because hand-bending dozens or hundreds of identical stirrups on site to consistent dimensions is slow and error prone. Our guide to ordering custom rebar stirrups covers dimensions, shape codes and what to put on the order.
Dowels tie one pour to the next: footing to wall, wall to slab, or new concrete to existing. Straight dowels are simple cuts; L-shaped or hooked dowels add a bend. Because they are short and numerous, they also have a high piece count per tonne. Dowels into existing concrete that are drilled and epoxied are a separate installation question for the engineer.
Cages. Some footings, piers and columns use assembled cages rather than loose bars. A pre-assembled cage moves tying labour from site to shop, which changes where the cost sits rather than removing it. See prefabricated rebar cages for footings and piers.
How to keep fabrication costs down
You can't change the design to save money without the engineer, but there is a lot you can do on the ordering side:
- Send complete, current drawings. Most re-work comes from fabricating to an old revision.
- Get the bar list approved before release. Questions answered on paper cost nothing; questions answered on site cost bent steel.
- Release by pour, not by the bar. Group the order into sensible phases that match the schedule.
- Give accurate site and delivery details. A truck that can't get in, or a second trip for a missed bundle, adds cost.
- Ask about standard shapes. Where the designer is flexible, standard shapes and consistent dimensions are quicker to make.
- Keep tags on until the steel is placed. Lost tags turn a 10 minute pick into an hour of measuring bars.
The step-by-step process for releasing an order is covered in how to order cut and bend rebar.
Shop fabrication vs site cutting and bending
Some contractors buy straight stock and do their own cutting and bending. That can work on small jobs with simple shapes. On larger jobs, compare the full cost: labour, equipment, waste from cutting stock lengths, the time to sort and identify pieces, and the risk of bends that don't meet the drawings. Shop fabrication moves that work onto shop bending equipment and hands your crew finished, tagged pieces.
Get a fabrication quote
We cut and bend 10M to 55M bar in our shop to all standard shapes, then tag and bundle it so your crew can place it without sorting. We also prepare estimates, bar lists and placing drawings from your structural drawings. Send us your drawings or bar list for a free take-off and quote, and see our services for detailing, fabrication, delivery and installation.
Frequently asked questions
What is rebar fabrication?
Rebar fabrication is turning straight mill bar into the pieces a job needs: cutting to length, bending to shape, then tagging and bundling each bar mark so it can be placed from the drawings.
Why do stirrups cost more per tonne than straight bar?
Stirrups are small, light pieces with several bends each, so a tonne of stirrups is hundreds of individual pieces to cut, bend, count and tag. A tonne of long straight bar can be a couple of dozen pieces.
Is it cheaper to bend rebar on site?
Sometimes for a few simple bends, but rarely for a full job. Site bending takes labour and equipment, produces more waste, and has to meet the bend diameters and tolerances on the drawings.
How much does rebar fabrication add to the price of rebar?
It depends on the job. A bar list of long straight bars adds little; one full of small stirrups and ties adds much more. The fastest way to find out is to send the bar list or drawings for a quote.