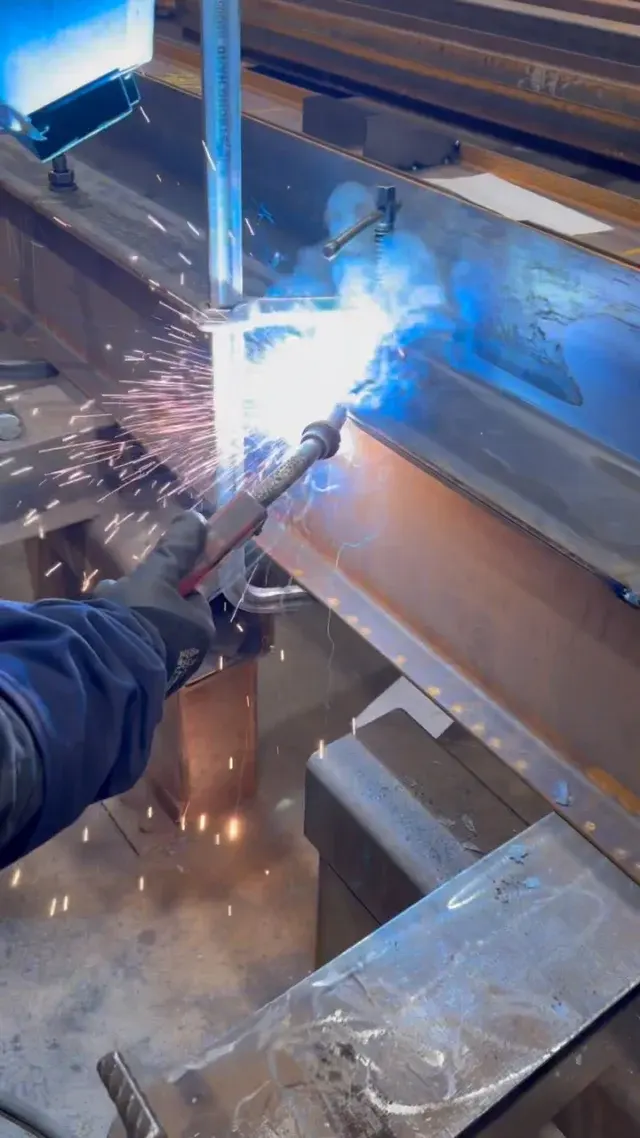
Coated rebar can be welded, but only when the engineer has designed the weld, the steel under the coating is a weldable grade such as 400W, and the work is done by a company certified to CSA W186. The coating is stripped from the weld zone before welding and repaired afterwards: galvanized bar to ASTM A780, epoxy-coated bar with the approved epoxy patching material. In practice most designers avoid welding coated bar and use laps or mechanical couplers instead, because every weld creates a corrosion weak spot in exactly the bar that was coated to resist corrosion.
The basics of which uncoated bar is weldable, and why most bar is tied, are in our post on weldable rebar in Canada. This post picks up from there: coated bars, what a rebar welding detail needs to show, and what to check before anyone strikes an arc.
Can it be welded? The short answer by bar type
| Bar | Weldable? | What has to happen |
|---|---|---|
| Black 400W or 500W | Yes, to a W186 procedure | Engineer's detail, certified company, qualified welder |
| Black 400R or 500R | Not intended for welding | R grades have no carbon equivalent limit; ask the engineer |
| Galvanized (zinc coated) | Yes, with extra steps | Weldable grade underneath, zinc removed, fume control, A780 repair |
| Epoxy-coated | Yes, with extra steps | Weldable grade underneath, coating removed, approved patching, damage limits |
| GFRP (fibreglass) | No | Not steel; use laps or GFRP-specific details |
The coating does not change the grade of the bar. A coating standard such as ASTM A767 (galvanizing) or ASTM A775 (epoxy) sits on top of a bar standard such as CSA G30.18. If the bar underneath is 400R, coating it does not make it weldable. Check the mill test certificate for the bar grade before assuming anything.
What a rebar welding detail should show
When a drawing calls for welded reinforcement, the welding detail is a design document, not a field note. A complete detail tells the welder and inspector:
- The bars being joined: size, grade and coating, for example "15M 400W, epoxy-coated".
- The joint type: bar to bar (a butt joint or a lap weld), bar to a splice member, or bar to structural steel such as an embed plate or anchor.
- The weld size and length, or the force the joint must develop so the W186 procedure can be matched to it.
- Shop or field. Shop welding gives better access, position and control. Field welding on coated bar also means coating repair in the field.
- Coating removal and repair, named by standard or product, so it is priced and not argued about later.
- Inspection and testing required by the specification.
If any of those are missing, raise a request for information before fabrication. A welder cannot fill gaps in a structural detail by judgement, and a W186 company will not weld without an accepted procedure for that joint.
CSA A23.1 sends welding of reinforcement, including tack welding, to CSA W186. W186 certification is run by the Canadian Welding Bureau, and it is separate from CSA W47.1, which certifies companies that weld structural steel. A shop certified for beams and columns is not automatically certified for rebar. Our post on CSA W59, the structural welding code explains how the welding standards fit together.
Welding galvanized rebar
Galvanized bar adds two problems to an ordinary rebar weld: the zinc gets in the way of a sound weld, and burning zinc gives off fumes.
Remove the zinc first. The American Galvanizers Association, citing American Welding Society guidance, says the zinc should be removed from roughly 25 to 100 mm (1 to 4 in.) on either side of the weld, on both sides of the work, with grinding as the most effective method. Welding through the coating risks porosity and cracking in the weld.
Control the fumes. Zinc fumes from welding can cause metal fume fever. Work in well ventilated areas, use local extraction or respiratory protection where ventilation is not enough, and treat confined spaces such as deep pits or forms with extra care. Your company's hot work and respiratory protection programs apply.
Repair the coating. A weld destroys the zinc at the joint and damages it next to the joint. The repair standard for galvanized coatings is ASTM A780, which covers zinc-rich paint, zinc-based solder and sprayed zinc. Zinc-rich paint is the usual site method. The specification should state the method and the required thickness.
Consider welding before galvanizing. Where a welded assembly is unavoidable, some specifications have it welded as black bar and then galvanized, so the zinc covers the weld. That only works if the assembly fits the galvanizer's kettle and the bending and coating sequence has been planned with the engineer. Our post on galvanized rebar specs covers A767 and A1094 bar and when bars are bent before or after coating.
Welding epoxy-coated rebar
Epoxy is a thin plastic film. Welding heat burns it at the joint and blisters or debonds it some distance away, and weld spatter burns small holes in the coating of nearby bars.
The practical rules:
- Strip the coating at the joint so the weld is made on clean steel, then patch everything the heat touched.
- Protect neighbouring bars from spatter with welding blankets. A spatter burn is coating damage and has to be patched like any other.
- Patch with the approved material. RSIC practice calls for coating and patching materials meeting OPSS 1443, or ASTM A775 and D3963, plus any local specification. General-purpose paint does not qualify.
- Watch the damage limit. Under RSIC practice all visible damage is patched and the total repaired area must stay below 2% of the bar's surface area per metre. Weld zones count toward that. Our epoxy-coated rebar touch-up guide covers the patching steps and when a bar should be replaced.
- Check the ground clamp location. Clamping onto coated bar damages the coating too, and arcing where the clamp makes poor contact leaves burns.
Bars coated to ASTM A934, which are coated after bending, are even less forgiving, because the coating is not designed to be disturbed after it is applied.
Why couplers and laps usually win
Welding coated bar is possible, but it is rarely the best detail. Compared with a lap splice or a mechanical coupler, a welded splice in coated bar needs:
- a W186 certified company on site, with qualified welders and an accepted procedure;
- coating removal, then coating repair that has to cure before concrete is placed;
- fume and fire controls in what may be a congested, enclosed formwork area;
- inspection of the weld and of the coating repair.
That is why many designers specify lap splices for coated bar where there is room and mechanical couplers where there is not. Where couplers are used on coated bar, the specification should say how the coupler is protected and how exposed steel at the joint is repaired. Our comparison of rebar couplers vs lap splices explains how the choice is made.
Tack welding coated cages: don't
The most common unauthorized weld on a job is a tack weld to stiffen a cage or a mat before it is lifted. On coated bar that is wrong twice over. CSA A23.1 treats tack welding as welding that must follow CSA W186, and a tack burns the coating at a point that will be buried in concrete. Coated cages are tied, normally with coated or non-metallic tie wire; see our post on rebar tie wire sizes, galvanized and coated. If a cage needs to be stiffer for lifting, ask the engineer for temporary bracing or lifting details.
A checklist before anyone welds coated bar
- The weld is shown on the structural drawings or accepted in writing by the engineer.
- The mill certificate confirms a W grade under the coating.
- The welding company holds CSA W186 certification, and the welder is qualified for the procedure.
- The coating removal method and distance are agreed.
- Fume control and hot work precautions are in place.
- The coating repair standard or product is named (ASTM A780 for zinc, the approved epoxy patch for epoxy).
- Neighbouring bars are protected from spatter.
- Inspection of the weld and of the coating repair is booked before the pour.
Getting bar for welded and tied details
We supply black steel rebar from 10M to 55M and GFRP bar, detailed, cut, bent, tagged and bundled to your bar list, along with fabricated dowels and stirrups. We do not supply galvanized or epoxy-coated rebar. If your drawings include welded details in black bar, flag them when you send the drawings so the bar grade and detailing are set up correctly from the start. Send your drawings for a free take-off and quote, or see our services.
Frequently asked questions
Can you weld galvanized rebar?
Yes, if the engineer has detailed the weld, the bar under the zinc is a weldable grade, and a company certified to CSA W186 does the work. The zinc is removed from the weld zone first, fumes are controlled, and the weld area is repaired to ASTM A780 afterwards.
Can you weld epoxy-coated rebar?
Only where the design calls for it and the coating specification covers the repair. Welding heat destroys the epoxy at and around the weld, so the coating is removed at the joint and every damaged area, including spatter burns on nearby bars, is patched with the approved epoxy patching material.
Can you tack weld coated rebar cages together?
Not as a substitute for tying. Tack welding is welding under CSA A23.1 and has to follow CSA W186, and on coated bar it also burns the coating. Coated cages are normally tied with coated or non-metallic tie wire.
Can fibreglass (GFRP) rebar be welded?
No. GFRP bar is a glass fibre and resin composite, not steel, so it cannot be welded. Connections are made with laps, bent bars or mechanical anchors designed for GFRP.