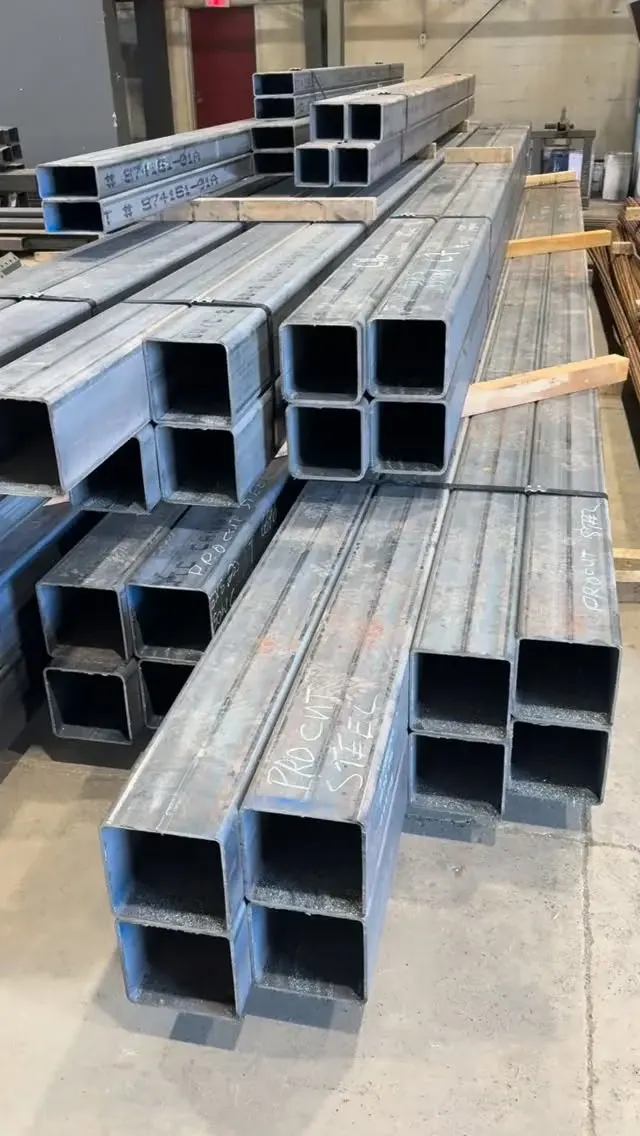
Yes, HSS steel can be welded. Hollow structural sections (square, rectangular and round steel tube) are made from weldable carbon steel, and they are welded every day into posts, columns, frames, trusses, canopies and railings. What changes with tube is the joint: you can only weld from the outside, the walls are often thin, and the face of the tube flexes, so fit-up, joint details and heat control matter more than on a solid beam. For structural work in Canada, the welds are made to CSA W59 by a company certified by the Canadian Welding Bureau.
A quick note on the term: in construction, HSS means hollow structural section. If you searched for welding high-speed steel, the tool steel used in drill bits and cutting tools, that is a different subject entirely. This post is about structural tube.
Can you weld HSS steel? Grades and weldability
The common HSS grades in Canada are CSA G40.21 350W (Class C or Class H) and ASTM A500 Grade C, with ASTM A1085 also available. All are carbon steels intended for welded construction. Our post on HSS steel grades in Canada covers the differences, including what Class C and Class H mean.
Two features of how tube is made affect welding:
- The seam weld. Most HSS is formed from flat strip and welded along its length (electric resistance welding). The seam is usually on one face of a square or rectangular tube, and there may be a small bead inside. It rarely matters for welding to the outside, but it can interfere with a plate or tube slid inside, and fabricators avoid putting a tight slip fit against it.
- Cold-formed corners. Class C and A500 tube are formed cold, so the corners are heavily worked and carry residual stress. Designers keep this in mind for details that weld into the corner region, and for galvanized or fatigue-loaded work they may specify the class of tube or particular precautions. Follow what the drawings and specification call for.
Who can weld structural HSS in Canada
The building code does not name the welding standards directly. The chain runs through the steel design standard: the 2024 Ontario Building Code requires structural steel to be designed to CSA S16, and S16 requires welded construction to CSA W59, by fabricators and erectors certified to CSA W47.1 by the Canadian Welding Bureau. Our post on CSA W59 explains the details.
In practice that means:
- the company holds CWB certification, with a welding engineer and supervisors on record
- welders are qualified for the process and positions they weld
- welds follow approved welding procedures; see our post on welding procedures (WPS and WPDS)
You can check a company's CWB certification before you award the work. A handrail post welded in a garage is not the same thing as a structural column connection, and the code treats them differently.
What makes tube joints different
On a W-beam you can usually reach both sides of a plate. On a tube you cannot, and the joint geometry changes around the perimeter.
Tube to plate
The most common HSS welds are tube to plate: base plates, cap plates, shear tabs and knife plates. They are usually fillet welds all around the tube. Points to get right:
- Square cuts. A tube cut off square sits flat on the plate. A cut a degree out leaves a gap on one side and a post that leans.
- Fit-up. Plates are tacked square to the tube before welding. On a tube, a tab a few degrees off throws the connected beam or brace off line.
- Weld size and wall thickness. On thin-walled tube, a large fillet adds heat without adding strength, because the tube wall becomes the limit. Weld sizes come from the design, and the procedure has to suit the wall.
Tube to tube
In trusses, frames and railings, branch tubes are welded directly onto a main tube (the chord). Our post on HSS connections and framing names the joint types (T, Y, K, N and X). For welding, what matters is the fit of the branch end:
- Square and rectangular branches are cut straight or bevelled to sit on the flat face of the chord.
- Round branches need a curved fish-mouth profile, cut to fit the curve of the chord. Shops cut these on a profile cutter or with templates.
- Width ratio. When a square branch is narrower than the chord, its sides land on the flat face and are fillet welded. When the branch is the same width as the chord, its sides land on the rounded corners, and the side welds become flare groove welds into the corner radius. The joint detail and weld type change, which is why the designer chooses member sizes with the connection in mind.
- Changing angle around the joint. Where a branch meets the chord at an angle, the angle between the two surfaces changes as you go around the branch: on the heel side it is obtuse, on the toe side it is acute. Prequalified details account for this, and the welder has to adjust technique around the joint.
Thin walls, heat and distortion
Many residential and miscellaneous tubes have thin walls. Welding them well comes down to heat control:
- Burn-through. Too much current or too slow a travel speed on a thin wall can melt through it. The procedure sets the process, consumable, current and travel speed for the wall thickness.
- Process choice. Gas metal arc and flux-cored arc welding are common in the shop for tube; shielded metal arc (stick) is used in the field and for repairs. Our comparison of structural welding processes covers how they differ.
- Distortion. Welding all the way around one end of a long tube, or along one face, pulls it out of straight. Shops balance welds, sequence them and use fixtures to keep frames square.
- Cleanliness. Mill scale, oil, paint and galvanizing are removed from the weld area first.
None of this is a recipe for structural welding at home. Structural welds need a qualified procedure and a qualified welder, and the connection itself needs an engineer's design.
Sealing, venting and galvanizing
Water inside a closed tube is a problem: it rusts the tube from inside and can freeze and split it. Typical practice:
- Exterior posts and columns are capped and based with welded plates all around, so they are sealed.
- Tubes to be hot-dip galvanized cannot be sealed. Molten zinc has to flow in and out, and trapped air or moisture can cause a dangerous pressure build-up in the kettle. Vent and drain holes are added, sized and located to suit the galvanizer and approved by the designer.
- Interior members are often left open-ended or capped for appearance.
We can prime or galvanize HSS to suit the job, so tell us the finish when you request a quote, and we will detail the vent holes or seal welds accordingly.
Inspection and appearance
All structural welds are inspected visually, and the specification may call for further testing on critical joints. Our post on structural weld defects and inspection covers what is checked. On HSS, inspectors look particularly at:
- weld size and full wrap-around on all-around fillets
- undercut on thin walls
- fusion at the start and stop of all-around welds, where the weld overlaps itself
- the flare welds at corners on matched-width joints
Exposed tube, such as a feature column, canopy or railing, often has appearance requirements: ground welds, consistent profiles, no spatter. Those need to be on the drawings before fabrication, because grinding and finishing add shop time.
Have your HSS fabricated
We fabricate HSS posts, columns and frames with base, cap and connection plates welded in our CWB certified shop, and we prepare the shop drawings in-house. Send your drawings through our quote request, or see our steel products for posts, plates and beams.
Frequently asked questions
Can you weld HSS steel?
Yes. Hollow structural sections in grades such as CSA G40.21 350W and ASTM A500 Grade C are weldable carbon steels, and tube is welded routinely for posts, frames, trusses and railings. Structural welds in Canada are made to CSA W59 by a CWB certified company.
Is HSS the same as high-speed steel?
No. In construction HSS means hollow structural section: square, rectangular or round steel tube. High-speed steel is a tool steel used for drill bits and cutters. Welding high-speed steel is a specialized tooling job and has nothing to do with structural tube.
Do HSS columns need to be sealed?
Exterior or exposed tubes are usually closed with welded cap and base plates so water cannot get in and freeze. If the steel will be hot-dip galvanized, the tube needs vent and drain holes instead, located with the designer's approval.
Who is allowed to weld structural HSS in Ontario?
CSA S16, the steel design standard referenced by the Ontario Building Code, requires fabricators and erectors who weld structural steel to be certified by the Canadian Welding Bureau to CSA W47.1. The welds themselves are made to CSA W59.