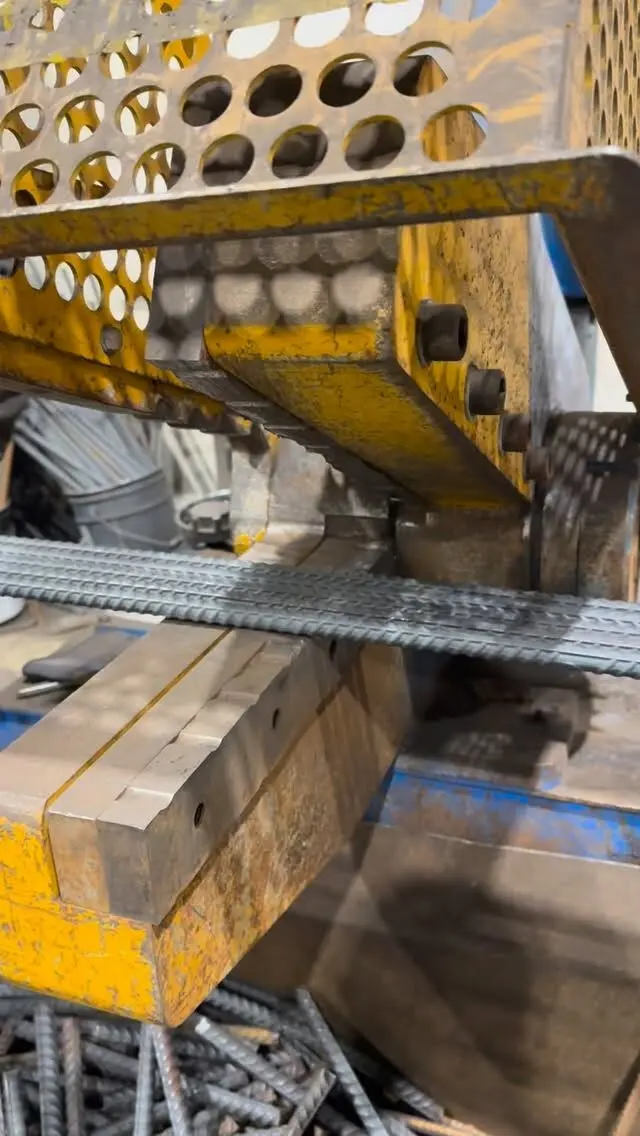
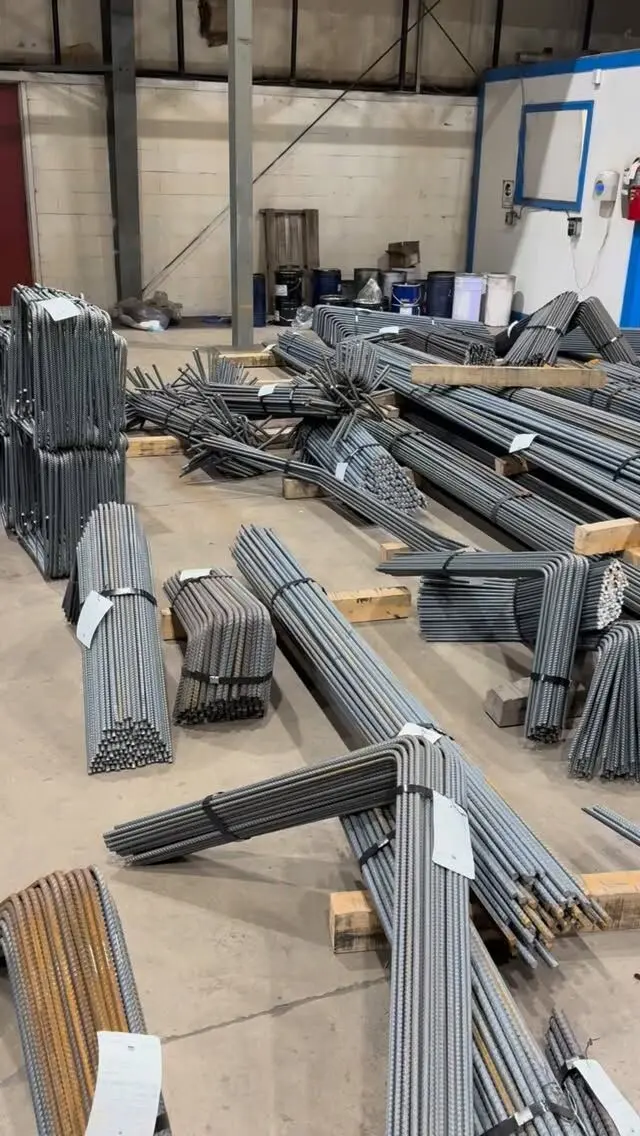
Yes, epoxy-coated rebar can be bent and cut, but the coating sets the rules. Bar coated straight to ASTM A775 is made to be cut and bent after coating, which a shop does with padded equipment and larger bend diameters than plain bar. Bar coated to ASTM A934 is bent first and coated afterwards, so it should not be rebent. On site, coated bar can be cut with a saw or shear, never a torch, and every cut end must be patched. Field bending is best avoided, and should only be done where the specification or engineer allows it.
The reason for all of this is simple: epoxy only protects the steel where the film is intact. Every bend stretches the film, and every cut leaves bare steel. Our comparison of epoxy-coated vs standard rebar explains how the coating works and when it is worth specifying.
A775 or A934: which bar can be bent?
The coating standard on the order tells you what can be done to the bar afterwards.
| ASTM A775/A775M | ASTM A934/A934M | |
|---|---|---|
| Sequence | Straight bar coated, then cut and bent | Bar cut and bent, then coated as finished shapes |
| Usual colour | Green | Purple or grey (manufacturer convention) |
| Bending after coating | Yes, that is how it is made | No; the shape is final |
| Cut ends | Exposed steel, must be patched | Coated, unless the bar is cut later |
| Late changes | Easier, since bending follows coating | Harder; a changed shape is a new piece |
With A775 bar, the coating is applied knowing it will be bent, and coating plant quality control includes bend tests to check its flexibility. With A934 bar, the coating goes onto the finished shape, so bending it again risks cracking the film and should be treated as off-limits unless the engineer and coating specification allow it.
Coated bar needs larger bend diameters
Because the outside of a bend stretches the coating, epoxy-coated bar is bent around larger pins than plain bar. The RSIC Manual of Standard Practice gives these finished bend diameters for hooks:
| Bar size | Plain bar, 400R/500R | Plain bar, 400W/500W | Epoxy-coated |
|---|---|---|---|
| 10M | 70 mm | 60 mm | 80 mm |
| 15M | 100 mm | 90 mm | 120 mm |
| 20M | 120 mm | 100 mm | 160 mm |
| 25M | 150 mm | 150 mm | 200 mm |
| 30M | 250 mm | 200 mm | 250 mm |
| 35M | 300 mm | 250 mm | 350 mm |
The hook extensions are longer too, so a coated hook takes more bar than a plain one. That has to be on the bar list from the start; a detailer working from plain bar tables will short every hook. Coated bar also needs longer development and lap lengths because the epoxy reduces bond. See epoxy-coated rebar lap length.
How coated bar is bent in the shop
Fabrication and handling of coated bar follow ASTM D3963/D3963M and, on Ontario provincial work, OPSS 905, which the RSIC manual points to. The shop has to change how it works:
- Padded contact areas. RSIC states that all contact areas must be padded when shearing, bending, banding, bundling, hoisting and shipping coated bar.
- The right pins. Bending to the coated bar table above, not the plain bar table.
- Patching in the shop. Sheared ends and fabrication damage are coated with an approved patching material.
- Careful bundling and lifting. Nylon slings, padded bands and enough support so bundles don't sag.
That is why the shop is the best place to bend coated bar. The process is controlled, the damage is visible on a flat bench, and patching happens before the bar leaves.
Field bending epoxy-coated rebar
Field bending of coated bar is best avoided. Small radius bends made with ordinary site benders crack the film on the outside of the bend, and the damage is easy to miss once the bar is tied in.
If the specification or engineer does permit a field bend, for example to fix a dowel position, treat it carefully:
- Confirm it is A775 bar. A934 shapes should not be rebent.
- Use a bender with padded or coated pins sized to the coated bar table.
- Bend cold, slowly and once. No heating, no straightening and rebending.
- Inspect the outside of the bend for cracks, disbonding or crushed coating.
- Patch everything you find before the concrete is placed.
Bars partly embedded in concrete need the engineer's approval before any field bend, coated or not. Our post on whether bending rebar weakens it explains why.
Cutting epoxy-coated rebar
Cutting is more common on site than bending, and the rules are straightforward:
- Use a saw or a shear. A portable rebar cutter or an abrasive saw both work. Pad the bar where it is clamped.
- Never use a torch. The heat burns and lifts the coating well beyond the cut, leaving bare, scorched steel along the bar.
- Patch every cut end. Clean the end as the patch manufacturer requires and apply the approved two-part repair epoxy, covering the cut face and any damaged coating around it.
- Let it cure before the bar is covered or placed in the concrete.
Plan as many cuts as possible into the bar list so they happen in the shop. Every field cut is another patch to get right and another spot for an inspector to check.
What a good repair looks like
RSIC practice is to patch all visible damage with an approved compound, following the patch manufacturer's instructions, and to keep the total repaired damage under 2% of the bar's surface area per metre. Bars damaged beyond that should be rejected. Project specifications can be stricter, and some add limits on bare spots or cut end treatment.
To keep repairs to a minimum:
- Store coated bar under cover. Ultraviolet light degrades the coating, and RSIC calls for covered storage.
- Don't drag bars or walk them across rough ground.
- Use coated or non-metallic chairs and tie wire.
- Ask for plastic-tipped vibrators. RSIC notes that studies have found most coating damage comes from vibrating concrete with uncoated vibrator heads.
Keep enough repair material on site for the whole job. Running out on pour day is a common reason damage goes unpatched. The submittal side of this is covered in epoxy-coated rebar submittals.
Getting coated bar detailed and supplied
The fewer cuts and bends made on site, the better coated bar performs. That means a complete bar list with coated hooks, laps and shapes worked out before fabrication, and a clear note of the coating standard.
We prepare bar lists and placing drawings from your structural drawings and cut and bend rebar from 10M to 55M. We supply black steel and GFRP bar rather than epoxy-coated bar, and can price either for your job if your designer allows it. Send your drawings, or see our services.
Frequently asked questions
Can epoxy-coated rebar be bent?
Yes. Bar coated to ASTM A775 is coated straight and then bent in the shop, using padded equipment and larger bend diameters than plain bar. Bar coated to ASTM A934 is bent before coating, so it should not be rebent. Field bending of coated bar is best avoided.
Can you cut epoxy-coated rebar on site?
Yes, with a saw or shear, never a torch. Every cut end exposes bare steel, so it must be patched with the repair material approved for the coating before the concrete is placed.
What bend diameter does epoxy-coated rebar need?
Larger than plain bar. The RSIC Manual of Standard Practice lists finished bend diameters for epoxy-coated hooks of 80 mm for 10M, 120 mm for 15M and 160 mm for 20M, compared with 60 to 70 mm, 90 to 100 mm and 100 to 120 mm for plain bar depending on grade.
How much coating damage is allowed on epoxy rebar?
RSIC practice is to patch all visible damage and to keep the total repaired area under 2% of the bar's surface area per metre. Project specifications can be stricter, so check yours.