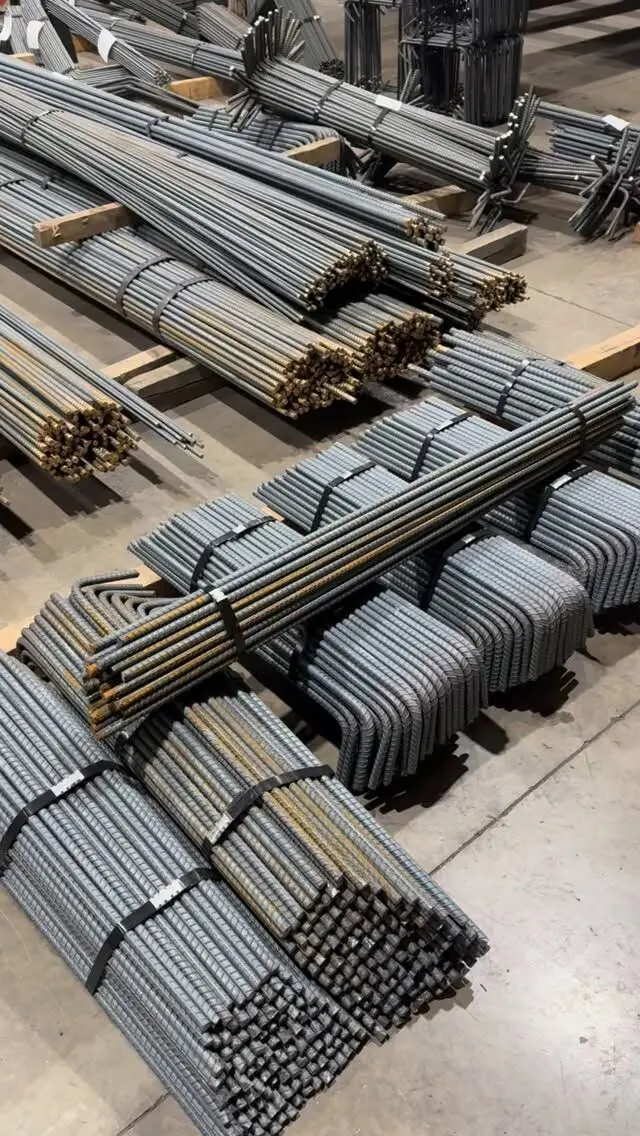
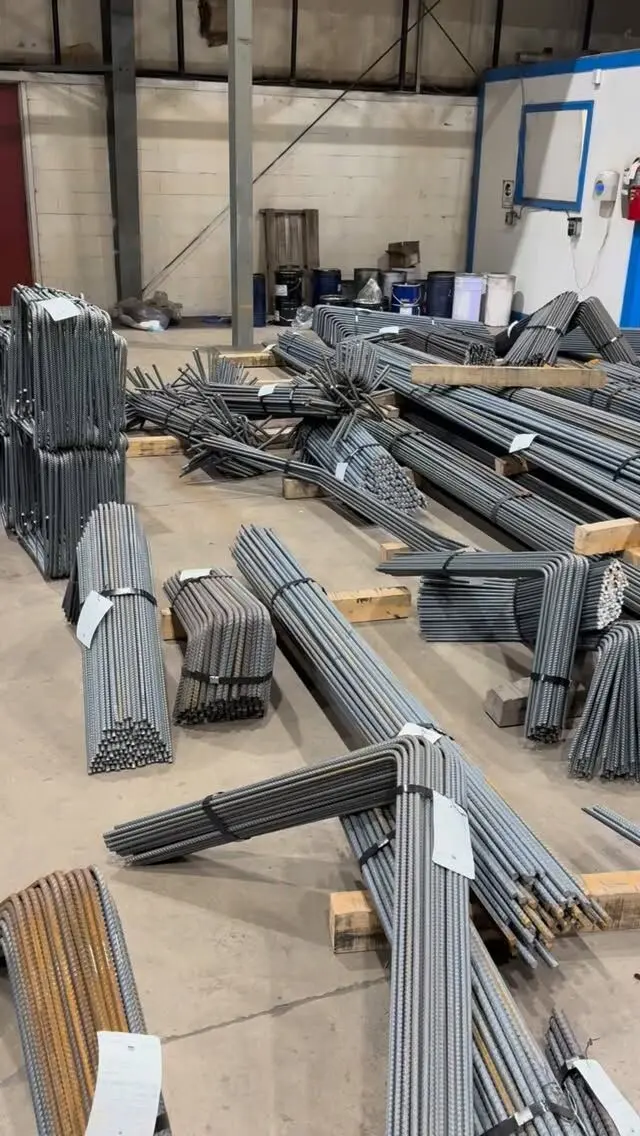
GFRP rebar is made by pultrusion: continuous glass fibre strands are pulled off spools, soaked in a thermosetting resin, shaped, and cured as they are pulled through a heated die. The bar comes out of the line as one continuous length and is cut to size at the plant. A surface treatment, such as a sand coating, a helical wrap or moulded ribs, gives it grip in concrete. Bent shapes cannot be made this way, so they are formed separately at the factory and cured in their final shape.
How the bar is made explains most of what is different about using it: why it cannot be bent on site, why it is strong along its length but not across it, and why quality varies between products. Here is the process from raw materials to finished bar.
What fiberglass rebar is made of
A GFRP bar has three main ingredients:
- Glass fibres. Thousands of fine glass filaments grouped into strands called rovings. They carry the tensile load. The 2019 edition of CSA S807 limits glass-fibre bars to E-CR glass, a corrosion-resistant type that better tolerates the alkaline environment inside concrete, and Ontario's Ministry of Transportation specifies E-CR glass for GFRP on its bridges.
- Resin. A thermosetting polymer that binds the fibres together, transfers load between them and shields them from moisture and alkali. CSA S807, the Canadian standard for FRP bars, covers polyester, vinylester and epoxy resins. Vinylester and epoxy are associated with the higher durability class.
- Additives and surface material. Curing agents that make the resin set, other additives that vary by product, and the sand or fibre wrap used to form the bonding surface.
Glass content is a big part of a bar's stiffness and strength. Specifications for demanding work set a minimum: MTO's provincial material specification for GFRP, for example, sets minimum glass content along with glass transition temperature and elongation limits. Manufacturers publish their own values on their data sheets.
Because almost all of the fibres run lengthwise, the bar is very strong in tension along its axis but much weaker across it. That is why GFRP behaves so differently from steel in shear, at bends and at cut ends. Our introduction to what GFRP rebar is covers how those properties play out in a structure.
The pultrusion process, step by step
Pultrusion is a continuous process for making composite profiles with a constant cross-section. The name combines "pull" and "extrusion": the material is pulled through a die rather than pushed. A rebar line works roughly like this:
- Creel. Many roving spools sit on a rack. Their strands feed into the line together, and the number of strands sets how much glass ends up in the bar.
- Guiding and tensioning. Guide plates keep the strands aligned and evenly tensioned so the fibres run straight in the finished bar.
- Resin impregnation. The strands pass through a resin bath, or resin is injected as they enter the die, so every filament is wetted out. Poor wet-out leaves dry fibres inside the bar, which hurts strength and durability.
- Preforming. The wet bundle is squeezed and gathered into a round shape, and excess resin is removed.
- Heated die. The bundle is pulled through a heated steel die that sets the final diameter. The heat triggers the resin's curing reaction, so the bar leaves the die as a solid.
- Surface treatment. The bonding surface is added at a point in the line that depends on the product: a fibre wrap wound around the bundle before it cures, ribs formed by the process, or a resin and sand layer applied to the bar and cured.
- Pulling. Clamps or tracks at the end of the line grip the cured bar and pull the whole bundle through the process at a steady speed.
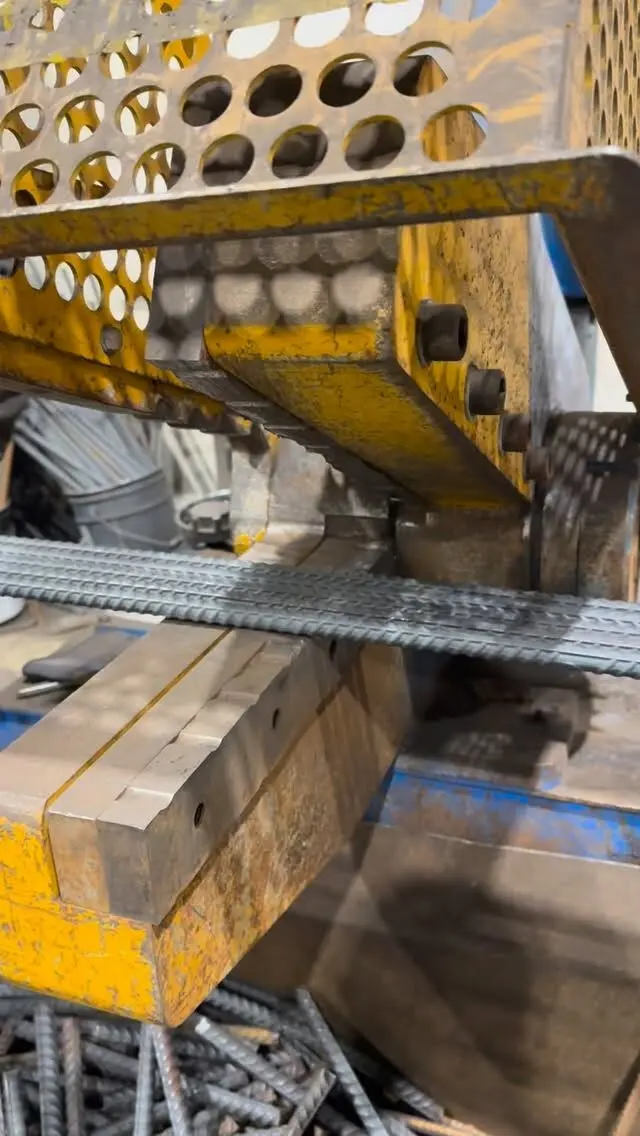
- Cutting. A saw cuts the continuous bar to the ordered lengths.
Line speed, die temperature and resin chemistry all have to be balanced. Pull too fast and the resin may not fully cure; that is the kind of defect that shows up later as poor durability rather than an obvious flaw on delivery.
Why GFRP bars from different makers look different
The surface treatment is where brands differ most. Some bars are sand-coated, some have a visible spiral wrap, some have moulded ribs, and colours vary. The surface affects bond with concrete, and it also explains why a bar's measured diameter is larger than its nominal size. Do not judge GFRP by appearance; judge it by the grade and test data.
How bent GFRP shapes are made
Standard pultrusion only makes straight bar. The resin is a thermoset, so once it has cured it cannot be softened and reshaped the way a steel bar can be cold-bent.
Bent bars, such as L-bars, U-bars, hooks and stirrups, are therefore made at the factory from bar that has not yet fully cured. The uncured bar is shaped on a form and then cured in that shape. That has three practical consequences:
- Every bend must be ordered in advance. A missing corner bar cannot be bent on site; it has to be made and shipped.
- Bends are weaker than straight bar. Fibres on the inside and outside of a bend are not as well aligned or loaded as in the straight bar, so the strength at a bend is significantly lower, and designs account for that.
- Bend geometry follows the manufacturer's capabilities. Bend radii and shapes for GFRP are not the same as steel's; use the manufacturer's data.
Our post on GFRP corners, L-bars and hooks goes into bent shapes in detail.
Quality testing and standards
In Canada, GFRP bars are made to CSA S807, which sets material and manufacturing requirements and test methods. Bars are graded by their minimum modulus of elasticity, with Grade III (60 GPa minimum) the stiffest, and are assigned a durability class, with D1 the higher class. Manufacturers test production for properties such as tensile strength and modulus, and qualify their products for longer-term behaviour.
Public owners add their own controls. MTO, for example, requires Grade III, durability class D1 bar from manufacturers on its Designated Sources for Materials list. On a private project, the equivalent is asking for the grade, durability class and test certificates that match the drawings. Our post on CSA S807 and S806 explains how the standards fit together.
What the manufacturing process means on site
How GFRP is made shows up in day-to-day handling:
- Bar list first. Bent shapes are made to order, so the bar list has to be complete and checked before production, and lead times are longer than for steel.
- Cutting. Straight bars are cut with a saw, and on MTO work only saw cutting with written permission is allowed. Cutting produces glass dust that calls for dust control and protective equipment; see how to cut fiberglass rebar.
- Lengths. The process is continuous, so length is limited by handling and shipping rather than by the line.
- Storage. The resin at the surface degrades with long exposure to sunlight, so bars stored on site should be covered.
For corrosion, conductivity and lifespan questions, see does fiberglass rebar rust.
Ordering GFRP rebar
We supply GFRP rebar alongside steel bar, detailed and tagged to your bar list, with bent shapes worked out before production. Send us your drawings for a quote, or see our rebar products.
Frequently asked questions
What is fiberglass rebar made of?
Continuous glass fibres, running along the length of the bar, held in a thermosetting polymer resin such as vinylester, epoxy or polyester. The surface is usually sand-coated, helically wrapped or ribbed so it bonds to concrete.
How is GFRP rebar made?
Straight bars are made by pultrusion: glass fibre strands are pulled from spools, soaked in resin, shaped and then cured as they are pulled through a heated die. The continuous bar is cut to length at the end of the line.
How are bent GFRP bars made?
Pultrusion only produces straight bar. Bent shapes are formed at the factory before the resin has fully cured and are then cured in their final shape. Once cured, a GFRP bar cannot be re-bent.
Why can't you bend fiberglass rebar on site?
The resin is a thermoset: once it cures it does not soften enough to reshape. Bending a cured bar breaks fibres and cracks the resin, so every bend has to be on the bar list before production.